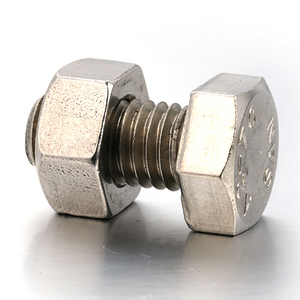
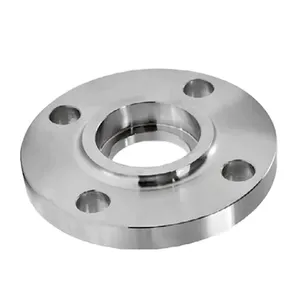
Direct-from-factory socket weld connections, high-pressure forged flanges, structural bolting, and hydraulic adaptors engineered to British and international pressure boundary standards.
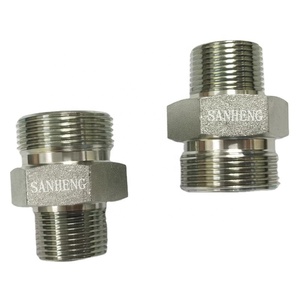
In high-consequence process piping systems across Great Britain, small-bore piping (typically DN 15 to DN 50 / ½″ to 2″) represents up to 35% of all field joints. Socket weld fittings provide superior pressure containment, structural rigidity, and zero-leak reliability compared to threaded alternatives.
Unlike buttweld connections requiring complex edge prep or threaded joints vulnerable to notch fatigue, socket weld fittings incorporate an internal counterbore. Pipe insertion with an obligatory 1.6 mm (1/16″) expansion gap prior to fillet welding prevents weld root thermal cracking during extreme temperature cycles, complying with ASME B31.3 Section 328.5.2.
Our closed-die forging process aligns grain structure parallel to fitting stress profiles. Material options span ASTM A105N normalized carbon steel for non-critical utilities, ASTM A350 LF2 Class 1 tested for sub-zero impact toughness at -46°C, austenitic stainless grades (A182 F316/316L), and UNS S31803 / S32750 Duplex for harsh marine chloride atmospheres.
Rated for working pressures exceeding 400 bar, our socket weld elbows (90° & 45°), equal/reducing tees, full couplings, half couplings, caps, and union fittings are manufactured strictly to ASME B16.11, MSS-SP-79, and British Standard BS 3799, seamlessly matching Schedule 80, Schedule 160, and XXS piping schedules.
Procurement reference for British structural engineers, M&E contractors, and pipeshop fabricators specifying ASME, BS, and EN compliant forged socket weld components.
| Component Type | Governing Specification | Available Size Range | Pressure Class | Standard Metallurgy | Certification |
|---|---|---|---|---|---|
| 90° & 45° Forged Elbows | ASME B16.11 / BS 3799 | 1/8″ – 4″ (DN 6 – DN 100) | 3000 lb, 6000 lb, 9000 lb | A105N, A350 LF2, A182 F316L | EN 10204 3.1 |
| Equal & Reducing Tees | ASME B16.11 / BS 3799 | 1/4″ – 4″ (DN 8 – DN 100) | 3000 lb, 6000 lb | ASTM A105N, A182 F51 / F53 | EN 10204 3.1 / 3.2 |
| Full & Half Couplings | ASME B16.11 / MSS SP-83 | 1/8″ – 4″ (DN 6 – DN 100) | 3000 lb, 6000 lb | A105, A350 LF2, F304L, F316L | EN 10204 3.1 |
| Socket Weld Unions | MSS SP-83 / BS 3799 | 1/4″ – 3″ (DN 8 – DN 80) | 3000 lb (Integral Seat) | Carbon Steel, SS 316 / Brass Seat | EN 10204 3.1 |
| Sockolets / Branch Outlets | MSS SP-97 | Outlet: 1/8″ – 4″, Run: up to 36″ | Class 3000, 6000 | A105, A350 LF2, A182 F11, F22 | PED / UKCA PER |
| Weld Neck & Socket Flanges | ASME B16.5 / BS EN 1092-1 | 1/2″ – 24″ (DN 15 – DN 600) | Class 150 – 2500 / PN 16 – 400 | A105N, A182 F316L, P250GH | EN 10204 3.1 / 3.2 |
Delivering high-specification forged socket weld components tailored to the UK's demanding geographic and regulatory operating environments.
Operated out of Aberdeen, Great Yarmouth, and the Shetland basin, offshore drilling rigs and FPSO modules demand extreme resilience against chloride stress corrosion. Our ASTM A182 F51 / F53 Duplex socket weld fittings provide verified PREn ≥ 40 for critical seawater injection, chemical inhibitor lines, and topside hydraulic manifolds.
In major chemical corridors like Teesside, Humberside, and Grangemouth, refining assets require ASTM A182 F11/F22 alloy and ASTM A105N normalized steel components. These handle continuous thermal cycles, hydrocarbon feedstocks, and high-pressure steam distribution without leak creep.
Backing the UK Net Zero 2050 targets, projects like HyNet North West and the East Coast Cluster require hydrogen-embrittlement-resistant, tight-tolerance Class 6000 socket weld fittings. We supply electro-polished stainless steels and certified low-porosity forgings that prevent micro-leakage in pressurized gas streams.
From Sizewell C and Hinkley Point C cooling auxiliaries to sterile pharmaceutical suites in Cheshire and Hertfordshire, our factory supplies fully documented dual-grade 316/316L forgings with controlled ferrite content, complete positive material identification, and clean-packaged seals.
Navigating post-Brexit regulatory demands, supply chain modernization, and decarbonization mandates within the British engineering market.
Following Brexit, mechanical piping components destined for UK pressurized assets must comply with the Pressure Equipment (Safety) Regulations 2016 (PER) and maintain compatibility with European PED directives. All our forged socket weld fittings are produced under approved ISO 9001 quality assurance programs with materials verified by certified Notified / Approved Bodies.
UK EPC contractors and stockholding distributors are shifting away from intermediate European traders to partner directly with audited manufacturing plants in China. Direct sourcing yields a 22–35% cost reduction on large capital projects, guarantees origin transparency, and provides customized forging runs according to precise project datasheets.
With both the EU CBAM and incoming UK CBAM targeting embodied carbon in ferrous imports, our manufacturing facilities utilize energy-efficient induction billet heating and modern closed-die hydraulic presses. We supply certified carbon accounting data alongside traditional MTCs to facilitate seamless customs clearance across UK ports.
Combining three decades of precision forging expertise with stringent quality management, comprehensive laboratory testing, and robust global export logistics.
Established in 1991, our production processes enforce individual heat-number hard stamping on every fitting, flange, and fastener. Each component ties directly to an authentic EN 10204 3.1 inspection certificate recording melt chemical analysis, tensile testing, Charpy V-notch impact values, and brinell hardness.
Equipped with high-precision multi-axis CNC lathes and broaching centers, we guarantee bore alignment within ±0.1 mm tolerance, perfectly square socket bottoms, and exact 1/16″ internal shoulder stops. This minimizes field fit-up time and ensures trouble-free orbital or manual stick welding on site.
Beyond socket weld fittings, our foundry and machining shops produce matching ASME B16.5 / BS EN 1092-1 forged flanges, buttweld fittings, and ASTM A193 B7/B8M high-tensile stud bolts. UK buyers streamline procurement through single-source containerized shipments directly to Felixstowe, Southampton, or London Gateway.
Addressing the core technical, compliance, and logistics questions raised by British engineering contractors, project managers, and quality inspectors.
Yes. Our tooling and quality matrices are built to meet both ASME B16.11 (covering Class 3000, 6000, and 9000) and British Standard BS 3799 specifications. Dimensions, pressure ratings, bore tolerances, and socket depths correspond directly with UK pipe schedules, ensuring seamless replacement and interoperability with existing North Sea or industrial infrastructure.
Every consignment includes EN 10204 Type 3.1 inspection certificates, detailing real chemical analysis, mechanical yield/tensile tests, Charpy impact test results (where specified for ASTM A350 LF2), and heat treatment histories. On request, independent third-party witnessing (Type 3.2 certification) by agencies such as Lloyd's Register, DNV, or TÜV can be arranged prior to export.
In environments susceptible to crevice corrosion or sour gas cracking, we supply socket weld fittings manufactured from low-carbon stabilized stainless steels (316L, 317L), 2205 Duplex, 2507 Super Duplex, or Nickel Alloys (Inconel 625, Hastelloy C276). All sour service materials undergo mandatory solution annealing and hardness verification in accordance with NACE MR0175 / ISO 15156.
Standard production runs for full container loads (FCL) or grouped LCL shipments are completed in 20 to 30 days. Transit time from Ningbo or Shanghai port to major UK container ports (Felixstowe, Southampton, or London Gateway) typically ranges from 28 to 35 days. For emergency shutdowns or urgent repairs, expedited air freight is available via Heathrow or Manchester.
Yes. We regularly undergo quality and vendor qualification audits by UK EPC contractors and major global oil operators. Our facilities hold ISO 9001, ISO 14001, and ISO 45001 accreditations, alongside international recognitions including Indian Boiler Regulations (IBR) and Engineers India Limited (EIL) approvals, attesting to our disciplined manufacturing standards.
Our dedicated engineering department and CNC turning cells produce bespoke socket weld fittings, specialized union adaptors, metric-to-imperial crossover fittings, and heavy-wall outlet connections to proprietary customer drawings, complete with custom beveling, threaded combinations, and internal bore profiling.
Connect directly with our engineering sales desk for full ASME B16.11 dimension charts, material test reports, and competitive factory-direct quotations for your next project tender.