
Girgaon, Mumbai, Maharashtra 400004, India [email protected] +91 9869506920
ASME B16.9 Buttweld Fittings Factory Stock by Rajtilak Metal India
Seamless and Welded ASME B16.9 Buttweld Pipe Fittings Ready for Inspection
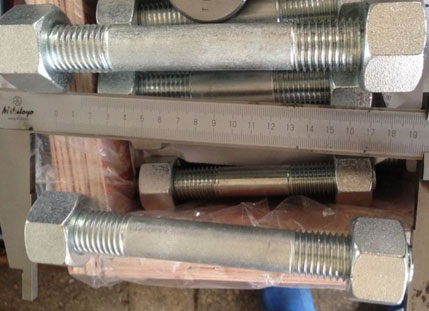
High Pressure Piping Materials and Stud Bolts Manufactured in India
ASME B16.9 buttweld fittings manufacturer warehouse in Mumbai India
1991Trusted Since
Precision Engineering & Global Supply

The Global Procurement Guide to ASME B16.9 Buttweld Fittings: Engineering Specifications, Material Selection, and Supply Chain Verification

In modern industrial piping networks across upstream hydrocarbon extraction, cryogenic LNG terminals, offshore platforms, and superheated steam generation, ASME B16.9 Buttweld Fittings constitute the vital circulatory backbone. Governed by the American Society of Mechanical Engineers, the ASME B16.9 standard establishes strict universal benchmarks for factory-made wrought buttwelding fittings covering sizes from NPS 1/2 through NPS 48 (DN 15 through DN 1200).

Rajtilak Metal, operating from Mumbai, India since 1991, stands as a premier Government of India Recognised Export House and an ISO 9001 certified manufacturer. Holding prestigious Indian Boiler Regulations (IBR) approval and Engineers India Limited (EIL) qualification, we produce high-yield buttweld components engineered to withstand high cyclic pressures, thermal expansion, severe hydrogen embrittlement risks, and abrasive multiphase flow.

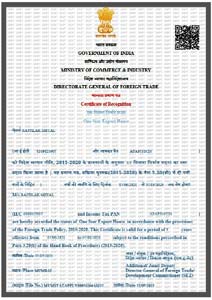
Government of India recognised export house accreditation
Stringent Quality Assurances for High-Risk Projects

All fittings are produced strictly matching host pipe schedule ratings from SCH 10 to SCH XXS. Shipped with fully traceable EN 10204 3.1 Mill Test Certificates and 100% heat-number integrity.

  • Dimensional, geometric tolerances, and weld-bevel preparation executed strictly per ASME B16.9 and ASME B16.25
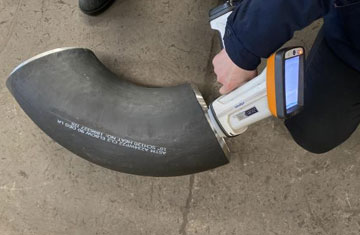
  • Complete in-house metallurgical verification: Positive Material Identification (PMI), Spectro analysis, and Charpy V-notch impact testing down to -196°C
  • Traceable prime feedstock sourced exclusively from audited primary steel mills across India, Japan, and South Korea
  • Specialty manufacturing for high-yield applications compliant with NACE MR0175 / ISO 15156 sour service
ISO 9001:2015 EIL Approved IBR Approved EN 10204 3.1

Contact Us

Product Spectrum

Recommended ASME B16.9 Buttweld Fittings by Critical Application

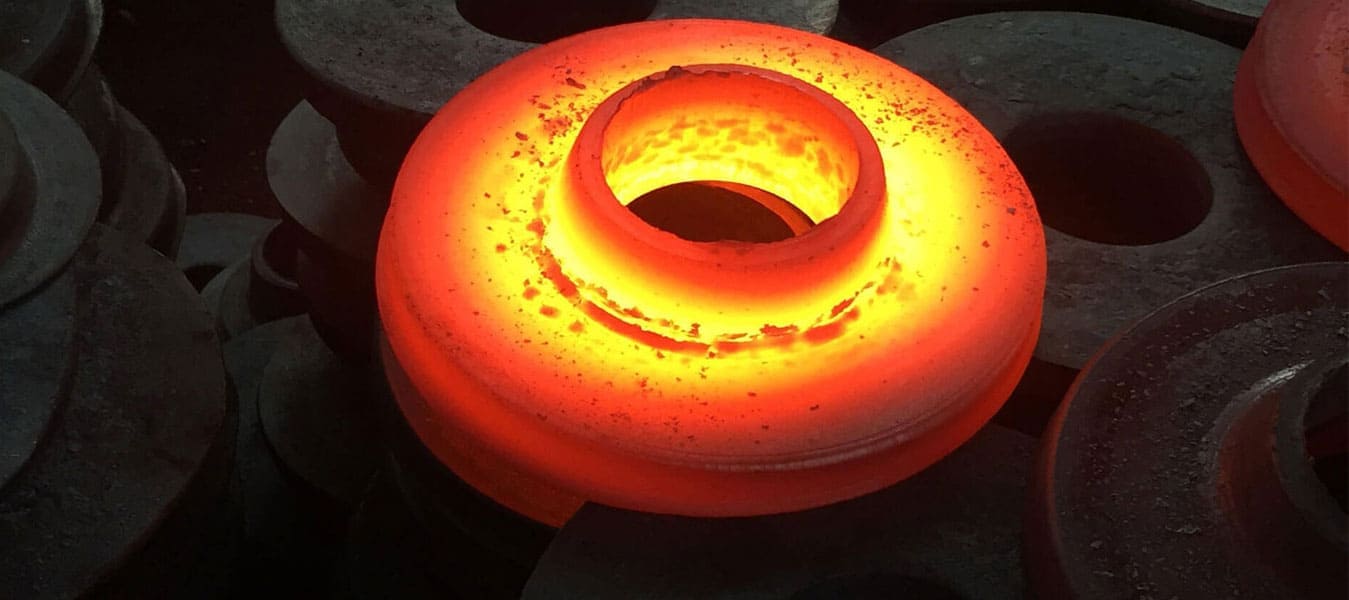
Our manufacturing program combines hot-mandrel forming, cold extrusion, hydraulic bulging, and state-of-the-art heat-treatment furnaces to engineer buttweld components that eliminate pressure drops and minimize internal turbulence.

ASME B16.9 Buttweld Long Radius and Short Radius Elbows

45°, 90°, 180° Buttweld Elbows (LR & SR)

Engineered for directional fluid control. Long Radius (R=1.5D) elbows optimize hydrodynamic velocity and suppress erosion, whereas Short Radius (R=1.0D) variants solve tight footprint constraints inside skid designs.

  • Seamless Execution: NPS 1/2″ to 24″ without seam factor derating
  • Welded Construction: NPS 26″ to 48″ with 100% X-ray radiographic testing
  • Wall Thicknesses: SCH 10S, SCH 40, SCH 80, SCH 160, SCH XXS
  • End Finish: ASME B16.25 bevel ends (37.5° ± 2.5° with 1.6mm root face)
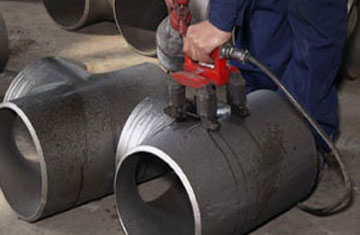
ASME B16.9 Equal and Reducing Tees Forging

Straight Equal, Reducing & Barred Tees

Designed for branch line distribution. Constructed with reinforced crotch profiles to prevent localized hoop stress peaks under surge pressure spikes in critical petrochemical applications.

  • Equal Tees: Branch diameter matches main header run
  • Reducing Tees: Smooth internal transitions avoiding fluid turbulence
  • Barred Tees: Custom internal guide bars for pipeline scraper pigging
  • Extruded Necks: Monolithic grain structures eliminating joint vulnerabilities
ASME B16.9 Reducers and Ellipsoidal End Caps

Reducers, Lap Joint Stub Ends & End Caps

Versatile pipeline components ensuring structural equilibrium when adapting pipe diameters, transitioning to floating flanges, or sealing high-pressure pipe manifolds permanently.

  • Concentric Reducers: Ideal for vertical lines and balanced fluid streams
  • Eccentric Reducers: Flat-side alignment preventing vapor lock in pumps
  • Lap Joint Stub Ends: Type A and B for loose backing flange assemblies
  • Ellipsoidal Pipe Caps: Deep-drawn pressure containment terminations
Engineering Excellence

Technological Evolution in Buttweld Fittings Manufacturing

From manual fabrication to smart hydraulic forming: Discover how state-of-the-art cold and hot forming methodologies redefine dimensional precision and grain continuity.

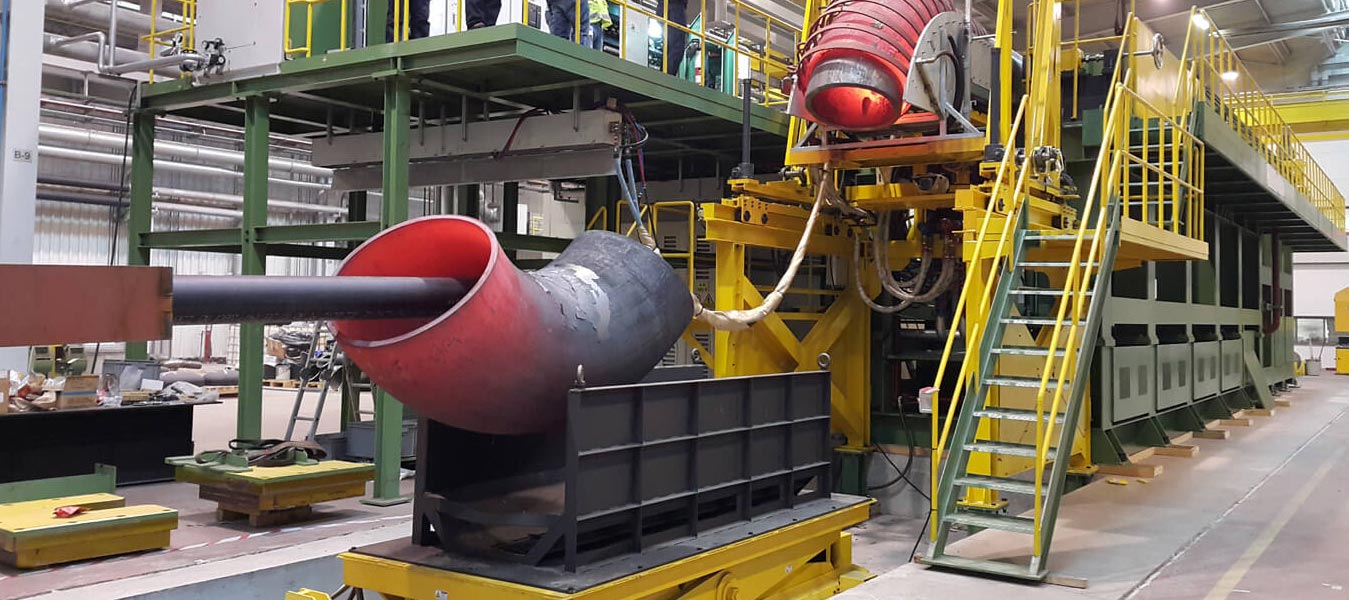
Hot Mandrel Induction Forming of Buttweld Elbows

Hot-Mandrel Induction Forming

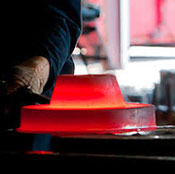
Our continuous hot-mandrel push benches heat seamless pipe billets gradually through high-frequency induction coils. This ensures uniform wall thickness on the extrados (outer radius) and avoids excessive thickening at the intrados, yielding elbows with optimal flow characteristics and zero residual stresses.

Computerized Hydroforming for Seamless Equal and Reducing Tees

Computerized Hydroforming

For austenitic stainless steels and duplex alloys, cold hydroforming utilizes extreme internal hydraulic pressure paired with horizontal mechanical punch movements. This pushes out seamless tee branches without introducing weld seams, guaranteeing structural homogeneity and preventing stress corrosion cracking.

CNC Beveling and Metrology Systems for Buttweld Ends

CNC Beveling & Laser Metrology

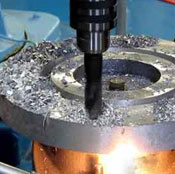
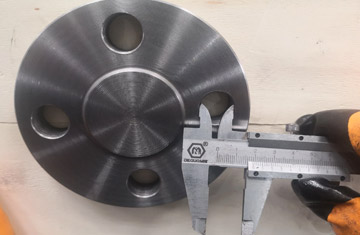
Welding failures on job sites frequently originate from uneven bevel lands. Rajtilak Metal employs multi-axis CNC end-finishing lathes guided by laser measurement systems to machine compound bevels to ASME B16.25 tolerances, allowing orbital automatic welding systems to achieve 100% first-pass weld acceptance.

Material Matrix

ASTM / ASME Material Grades for Buttweld Pipe Fittings

Matching the fitting's chemical formulation and mechanical yield capacity directly to connecting pipeline specifications ensures flawless field weldability and uniform pressure retention.

Comprehensive metallurgical standard cross-reference for factory-made ASME B16.9 buttweld fittings. Dual certification is standard for stainless grades.
Material Category ASTM / ASME Standard Common Grades Design Temperature Scope Target Process Environment
Standard Carbon Steel ASTM / ASME A234 WPB, WPC -29°C to 427°C (-20°F to 800°F) Refinery processing, non-corrosive hydrocarbons, high-pressure steam distribution
Low-Temp Carbon Steel ASTM / ASME A420 WPL6, WPL3 -46°C to -100°C (-50°F to -150°F) LPG/LNG gas processing, arctic pipelines, cryogenic refrigeration circuits
High-Yield Carbon Steel ASTM / ASME A860 / MSS SP-75 WPHY 42, 52, 60, 65, 70 -30°C to 120°C (-22°F to 250°F) High-pressure cross-country gas pipelines, offshore gathering systems
Austenitic Stainless Steel ASTM / ASME A403 WP304/304L, WP316/316L, 321H, 347H -196°C to 815°C (-320°F to 1500°F) Nitric/organic acid plants, marine atmospheres, food, pharma, clean energy loops
Duplex & Super Duplex ASTM / ASME A815 UNS S31803 (2205), UNS S32750 (2507) -50°C to 300°C (-58°F to 572°F) Seawater cooling, subsea manifolds, aggressive chloride & bleaching environments
Alloy / Chrome-Moly ASTM / ASME A234 WP11, WP22, WP5, WP9, WP91 Up to 650°C (1200°F) Boiler superheaters, catalytic cracking units, thermal power stations
Nickel Alloys & Titanium ASTM B366 / ASTM B363 Alloy 625, 825, C276, Gr. 2 Titanium Sub-zero to 1000°C Flue gas desulfurization, nuclear waste handling, hyper-corrosive chemicals
0+
Years of Manufacturing Experience
0%
Ultrasonic & PMI Tested Stock
0+
Export Countries Supplied
0.8%
First-Time Acceptance Rate
Enterprise Quality Architecture

Heat Number Integrity & Strict Non-Destructive Examination

Rajtilak Metal's engineering philosophy centers around the principle of total mechanical and chemical traceability. Every single ASME B16.9 buttweld fitting moving across our production floor carries a micro-stamped, permanent heat identity linking it directly with the original ladle analysis and furnace melt record.

Unlike standard commercial stockists, our manufacturing protocol incorporates a multi-tier Non-Destructive Examination (NDE) workflow. We maintain dedicated in-house metallurgical testing stations certified for liquid penetrant testing (PT), magnetic particle inspection (MPI), ultrasonic thickness and lamination testing (UT), and radiographic weld seam assessment (RT).

1
Melt Chemistry Assurance

100% PMI testing verifying Cr, Ni, Mo, and carbon equivalents.

2
Hot Forming Discipline

Controlled solution annealing and normalising thermal cycles.

3
Precision Bevel Control

Tolerances monitored to fractions of a millimeter per ASME B16.25.

4
Inspection Dossier

EN 10204 3.1 certification accompanied by full NDE test reports.

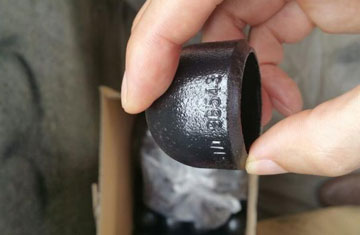
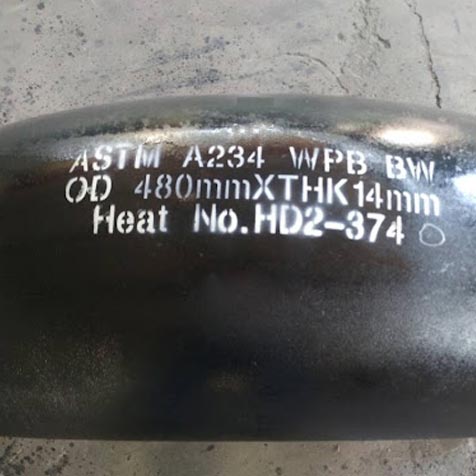
Clear Heat Number Markings and Traceability on ASME B16.9 Buttweld Fittings
Engineered for Extremes: India's Leading EIL & IBR Approved Piping Solutions Provider
The Rajtilak Metal Advantage

Why Major Global Engineering Contractors Rely on Us

Approved for Critical Service

As an Engineers India Limited (EIL) and Indian Boiler Regulations (IBR) approved manufacturer, our buttweld fittings and forgings are officially qualified for the world's most demanding refining, fertilizer, and petrochemical projects.

Comprehensive Materials Fleet

From commodity ASTM A234 WPB carbon steel to rare Hastelloy C276, Inconel 625, Monel 400, and Grade 2 Titanium, we maintain over 3,000 metric tons of mother pipe and hollow billets ready for fast-track custom fabrication.

Global Logistics & Packing

Exporting to over 50 countries across the Middle East, Southeast Asia, Europe, and the Americas. Packed in seaworthy ISPM-15 heat-treated wooden boxes with customized end caps to preserve weld bevel geometry completely intact.

From ADNOC onshore projects in the United Arab Emirates to power generation facilities in Southeast Asia and refinery maintenance hubs across Europe, Rajtilak Metal guarantees transparent lead times, competitive mill direct pricing, and uncompromising technical compliance. Click here to discuss your project requirements with our technical sales team.

Procurement Knowledge Base

Frequently Asked Questions on ASME B16.9 Buttweld Fittings

Authoritative technical answers to common questions raised by piping layout designers, QA/QC managers, and international procurement specialists.

What is the technical scope of ASME B16.9 versus ASME B16.11 and ASME B16.28?

ASME B16.9 covers factory-made wrought buttwelding fittings in sizes NPS 1/2 through NPS 48 for all pressure-temperature ratings matching the connected pipe schedule. In contrast, ASME B16.11 governs small-bore forged socket-welding and threaded fittings (typically NPS 1/8 to NPS 4) classified under definite pressure classes (Class 2000, 3000, 6000, 9000). ASME B16.28 was historically the standard for short radius elbows and returns, but this standard has been officially withdrawn and integrated directly into the unified ASME B16.9 specification.

Does ASME B16.9 designate explicit pressure-temperature ratings?

No. Unlike flanges governed by ASME B16.5 which have specific pressure classes (Class 150 to 2500), ASME B16.9 buttweld fittings derive their pressure rating directly from the matching straight seamless pipe of equivalent grade, wall thickness, and diameter. By standard definition, a fitting built to ASME B16.9 must be capable of withstanding 100% of the maximum design proof pressure that an uninterrupted straight pipe of identical schedule and metallurgy would sustain under ASME B31.1, B31.3, or B31.8 pressure piping codes.

What is the difference between Seamless and Welded ASME B16.9 fittings, and when is each mandatory?

Seamless buttweld fittings are formed directly from seamless mother pipe or solid forged billets without any longitudinal or circumferential weld seams, ensuring a weld joint quality factor (E) of 1.0. They are mandatory in high-cyclic, hyper-corrosive, or lethal process services. Welded fittings are manufactured from plate or welded tubulars, featuring one or two longitudinal weld seams. Welded fittings are common for large diameters (typically NPS 14 and above), requiring 100% radiographic examination (RT) or ultrasonic examination (UT) of all weld seams to ensure weld joint integrity equal to seamless constructions.

How are weld end bevels inspected and standardized under ASME B16.25?

Buttweld fitting ends are prepared to match the wall thickness of the mating pipe. For pipe wall thickness (t) up to 22 mm (0.88 in), the ends are prepared with a plain bevel angle of 37.5° ± 2.5° and a root face land of 1.6 mm ± 0.8 mm (1/16 in ± 1/32 in). For wall thicknesses exceeding 22 mm, a compound bevel is machined per ASME B16.25 to prevent excessive weld puddle buildup and optimize penetration during orbital TIG/MIG welding operations.

Can ASTM A234 WPB buttweld fittings be utilized in low-temperature service?

Standard ASTM A234 Grade WPB fittings are typically rated down to -29°C (-20°F). For temperatures below this threshold, ASTM A234 WPB cannot be used unless Charpy V-notch impact testing has been specifically executed and accepted per ASME Section VIII Division 1 guidelines. For verified cryogenic and low-temperature operations down to -46°C (-50°F), pipeline engineers mandate ASTM A420 Grade WPL6, which undergoes mandatory low-temperature impact testing during mill manufacturing.

What quality documents must accompany a shipment of ASME B16.9 fittings?

Every professional shipment must include a comprehensive inspection dossier containing the manufacturer's EN 10204 3.1 Mill Test Certificate (MTC), detailing chemical composition, heat treatment condition, tensile yield strength, elongation, and Brinell hardness. For critical applications, third-party inspection (TPI) endorsements (EN 10204 3.2), PMI reports, NDT non-destructive examination logs (RT, UT, PT, MPI), dimensional inspection reports, and certificate of origin endorsements by the Chamber of Commerce are supplied.

Direct Procurement Channel

Connect with Rajtilak Metal's Technical Piping Specialists

Whether you require fast-track delivery of ASTM A234 WPB elbows for refinery turnaround maintenance, custom heavy-wall ASTM A403 WP316L tees for a pharmaceutical expansion, or high-yield WPHY 60 reducers for long-distance oil transport, our technical engineering desk is available 24/7 to analyze your piping specification sheets and provide rapid, optimized commercial offers.

Contact us now to discuss material test plans (ITP), third-party inspection protocols, or to request our latest comprehensive product stock catalogs and dimension handbooks.

Contact Us
Comprehensive Inventory of Industrial Pipeline Components and Fasteners

Ready to Procure ASME B16.9 Buttweld Fittings?

Direct Email Dispatch[email protected]
International Sales Hotline+91 9869506920