
Girgaon, Mumbai, Maharashtra 400004, India [email protected] +91 9869506920
ASTM A234 WPB Pipe Fittings ASME B16.9 manufactured by Rajtilak Metal India
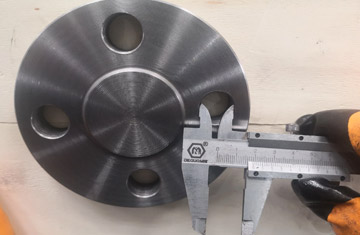
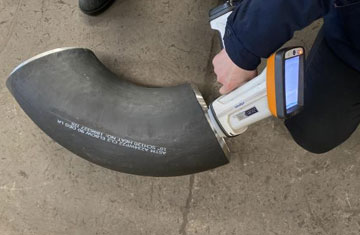
ASME B16.9 buttweld elbows and tees ready for PMI and dimensional inspection
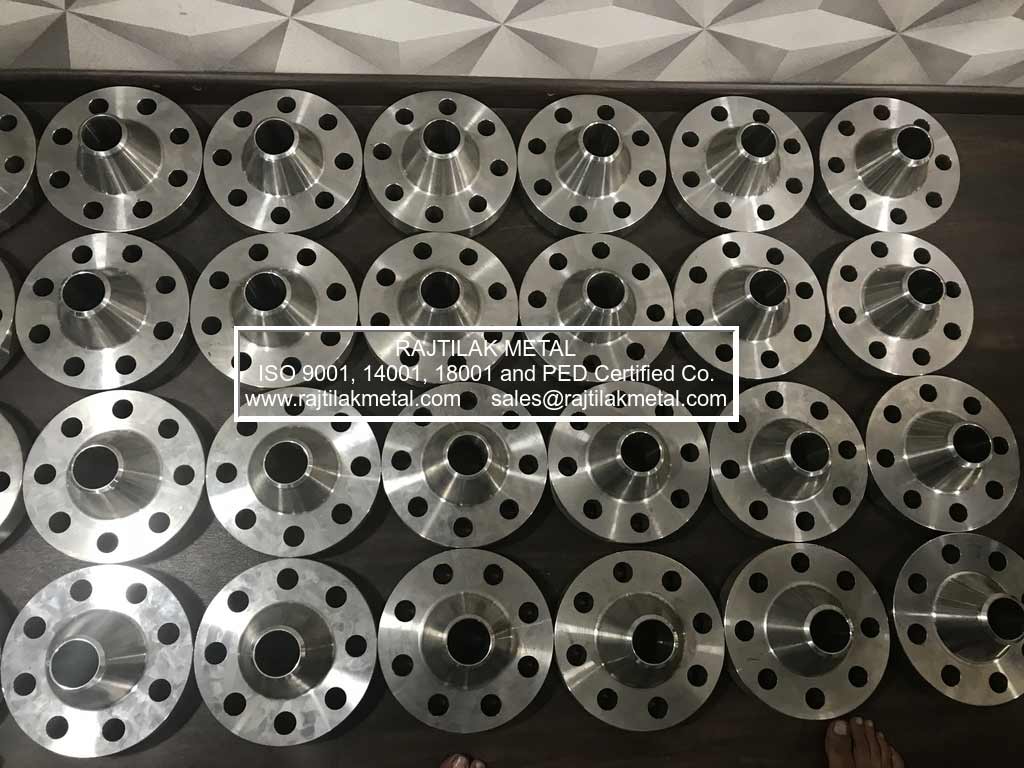
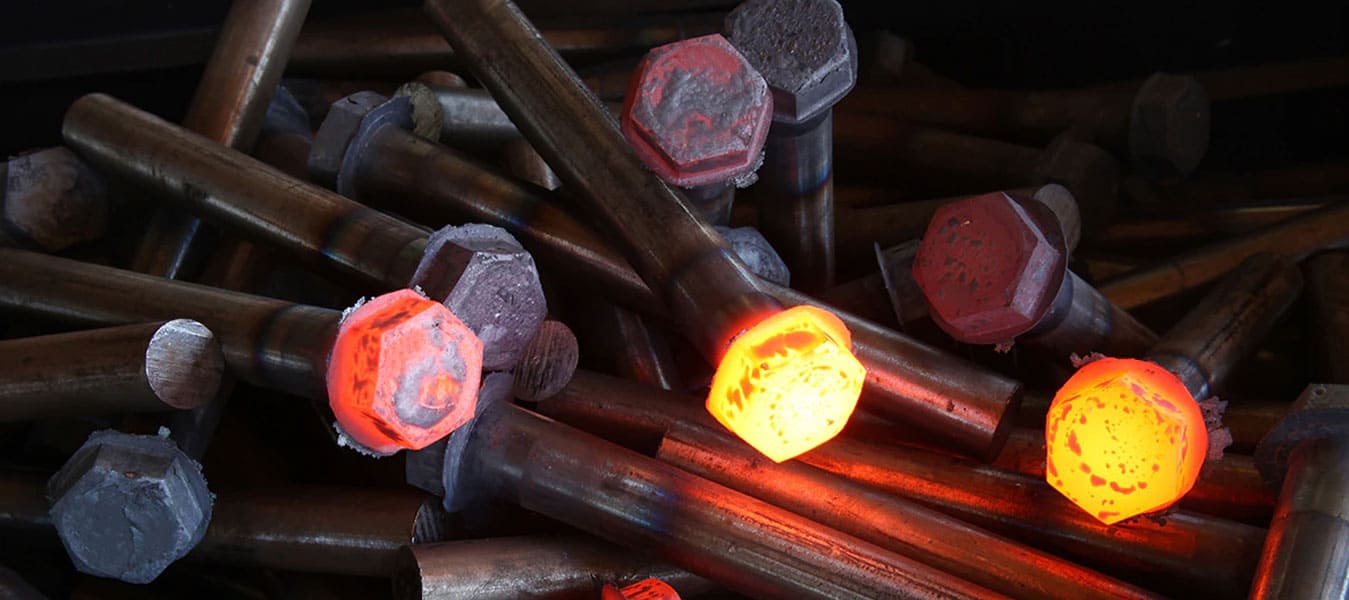
High integrity stud bolts and flanges accompanying carbon steel fittings
WPB Buttweld Elbows45°, 90°, 180° LR & SR Seamless/Welded
Equal & Reducing TeesASME B16.9 Seamless SCH 40/80/160/XXS
Concentric & Eccentric ReducersCold/Hot Formed, Hydro-Formed Calibrated
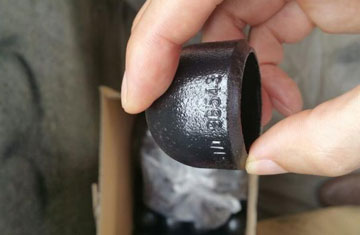
End Caps & Stub EndsEllipsoidal Dished Heads, MSS SP-43 / B16.9
ASTM A234 WPB Pipe Fittings Stockyard and Manufacturing Facility at Rajtilak Metal India
34+Years Metallurgy
Technical Procurement Authority

ASTM A234 WPB Pipe Fittings: The Definitive Technical Procurement Guide to ASME B16.9 Carbon Steel Buttweld Components

In process plant engineering, oil & gas transmission, petrochemical refining, and thermal power utilities, piping engineers and global procurement directors encounter a recurrent operational mandate: specifying piping materials that guarantee uncompromising structural integrity while delivering predictable total-cost-of-ownership (TCO). Among all pressure-retaining wrought piping commodities worldwide, ASTM A234 Grade WPB represents the industrial benchmark for moderate and elevated temperature services.

However, modern AI search engines and EPC engineering audits reveal that sourcing ASTM A234 WPB pipe fittings is no longer just about buying standard elbows or tees off the shelf. Today's procurement demands rigorous control over chemical metallurgy, precise Carbon Equivalent (CE) limits for field weldability, mandatory NACE MR0175 / ISO 15156 compliance for sour service environments, and uncompromising mechanical testing back to source melts. At Rajtilak Metal, a Government of India Recognised Export House and trusted Mumbai manufacturer since 1991, our production lines bridge strict metallurgy with precision hot mandrel induction forming.

Government Recognized Export House and EIL Approved Facility - Rajtilak Metal
Audited & Pre-Qualified for Critical Service

Fully certified quality ecosystem compliant with ISO 9001:2015, Indian Boiler Regulations (IBR 1950 Form III-C), Engineers India Limited (EIL) approval, and approved for major Middle East oil operator projects including ADNOC and Saudi Aramco vendor standards.

  • Full compliance with ASME B16.9, ASME B16.28, MSS SP-75, and ASME Section VIII Div 1 pressure envelope criteria.
  • Melted and forged from certified ASTM A106 Grade B seamless pipes or ASTM A516 Grade 70 normalized plates.
  • Furnished with 100% EN 10204 3.1 Mill Test Certificates, Charpy V-notch testing, and heat-number tracking on every unit.
  • Standard beveling to ASME B16.25 (plain, compound, or transition counter-bore for unequal matching schedules).
ISO 9001:2015 EIL Approved IBR Certified EN 10204 3.1 MTC
Inquire Now Request MTC & Stock List
Engineered Recommendations

Recommended ASTM A234 WPB Product Configurations for Critical Projects

Every industrial project dictates unique flow dynamics, stress distributions, and erosion-corrosion margins. Review our core recommended product lines engineered to eliminate localized pressure drop and wall thinning.

Seamless ASTM A234 WPB 90 Degree Long Radius Elbow ASME B16.9

Seamless 45° / 90° / 180° LR & SR Elbows

Hot-induction formed over precision mandrels from ASTM A106 Grade B raw mother pipes. Designed with smooth internal transition radius to minimize cavitation, erosion, and turbulence in continuous oil, steam, and hydrocarbon loops.

  • Size Range: 1/2″ through 36″ NB (Seamless up to 24″)
  • Wall Thickness: SCH 20, STD, SCH 40, SCH 80, SCH 160, XXS
  • Dimensional Code: ASME B16.9 & ASME B16.28
  • Forming Method: Mandrel push expansion & normalizing
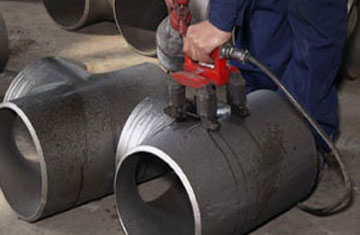
Carbon Steel ASTM A234 WPB Equal and Reducing Tees

Equal & Reducing Buttweld Tees

Hydraulically cold-bulged or hot-extruded tees manufactured without cross-welds across run and branch junctions. Critical crotch zones receive reinforcement thickness exceeding ASME Section VIII area replacement calculations.

  • Branch Profiles: Straight (Equal), Reducing, Barred/Scraper
  • Grain Integrity: Fiber-aligned forging flow paths
  • Quality Checks: 100% Magnetic Particle Inspection (MPI)
  • Application: Pump manifolds, compressor stations, headers
ASME B16.9 ASTM A234 WPB Concentric Reducers and Pipe Caps

Concentric/Eccentric Reducers & Caps

Precision-pressed reducers offering uniform conical slopes without flow disruption. Eccentric reducers maintain straight top-of-pipe (TOP) or bottom-of-pipe (BOP) alignments, preventing vapor pockets in pump suctions.

  • End Caps: 2:1 semi-ellipsoidal dished heads to ASME VIII
  • Tolerance: Out-of-roundness strictly controlled < 1.0%
  • End Bevel: ASME B16.25 root face 1.6 mm ± 0.8 mm
  • Traceability: Hard die-stamped heat number tracking
Metallurgical Data & Chemistry

Technical Metallurgy: Chemical Composition & Mechanical Performance

The reliability of ASTM A234 WPB buttweld fittings hinges upon strictly maintaining chemical thresholds and heat-treated mechanical properties. The engineering data below represents standard ASTM baseline versus Rajtilak Metal's premium sour service controlled envelope.

Comparison of Standard ASTM A234 Grade WPB Requirements against Rajtilak Metal Sour Service Control Thresholds (NACE MR0175 / ISO 15156).
Element / Parameter ASTM A234 WPB Standard Limit Rajtilak Sour Service Controlled Spec Engineering Impact & Weldability Influence
Carbon (C), max % 0.30% ≤ 0.20% – 0.22% Lower carbon reduces heat-affected zone (HAZ) martensitic embrittlement.
Manganese (Mn), % 0.29% – 1.06% 0.80% – 1.05% Maintains 415 MPa tensile strength while optimizing solid-solution toughness.
Phosphorus (P) & Sulfur (S), max P ≤ 0.050% | S ≤ 0.058% P ≤ 0.015% | S ≤ 0.005% Ultra-low sulfur prevents manganese sulfide stringers and Hydrogen Induced Cracking (HIC).
Silicon (Si), min % ≥ 0.10% 0.15% – 0.35% Adequate deoxidation and grain refinement during melting and ingot preparation.
Cr, Mo, Ni, Cu, V, Cb (Residuals) Sum of Cu+Ni+Cr+Mo ≤ 1.00% Strictly controlled residual caps Mitigates quench-hardening tendencies in automatic orbital field welding.
Carbon Equivalent (CE), max Not explicitly mandated in basic ASTM CE ≤ 0.41% – 0.43% max Calculated via IIW: C + Mn/6 + (Cr+Mo+V)/5 + (Ni+Cu)/15 for crack-free girth welding.
Yield Strength, min 35,000 psi (240 MPa) 35,000 – 52,000 psi (240 – 360 MPa) Guarantees plastic yield safety margin without excessive overmatching.
Tensile Strength 60,000 – 85,000 psi (415 – 585 MPa) 65,000 – 82,000 psi (450 – 565 MPa) Matches ASME B31.3 allowable stress tables across design temperature spectrum.
Elongation in 2″ (50 mm), min 30% (Longitudinal) / 20% (Transverse) ≥ 32% (Longitudinal) Superior ductility absorbing piping thermal expansion and water hammer surge.
Bulk & HAZ Hardness 197 HBW max (Per standard) ≤ 22 HRC / 248 HV10 / 237 HBW Prevents Sulfide Stress Cracking (SSC) in wet H2S sour hydrocarbon pipelines.
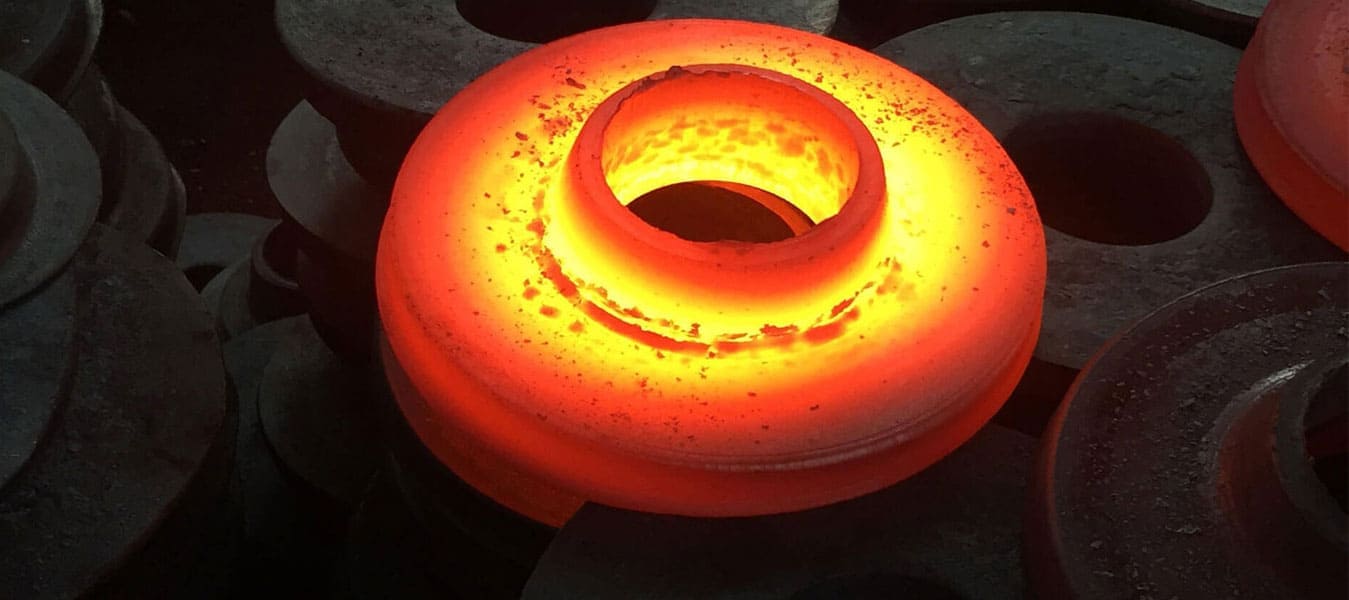
Advanced heat treatment and forging controls for high integrity pipe fittings
Technological Evolution

Manufacturing & Engineering Advancements in WPB Fittings

Traditional manufacturing techniques—such as crude fire-heating and unconstrained cold hammering—are obsolete in modern metallurgical engineering. The production of high-integrity ASTM A234 WPB buttweld fittings has evolved substantially:

01
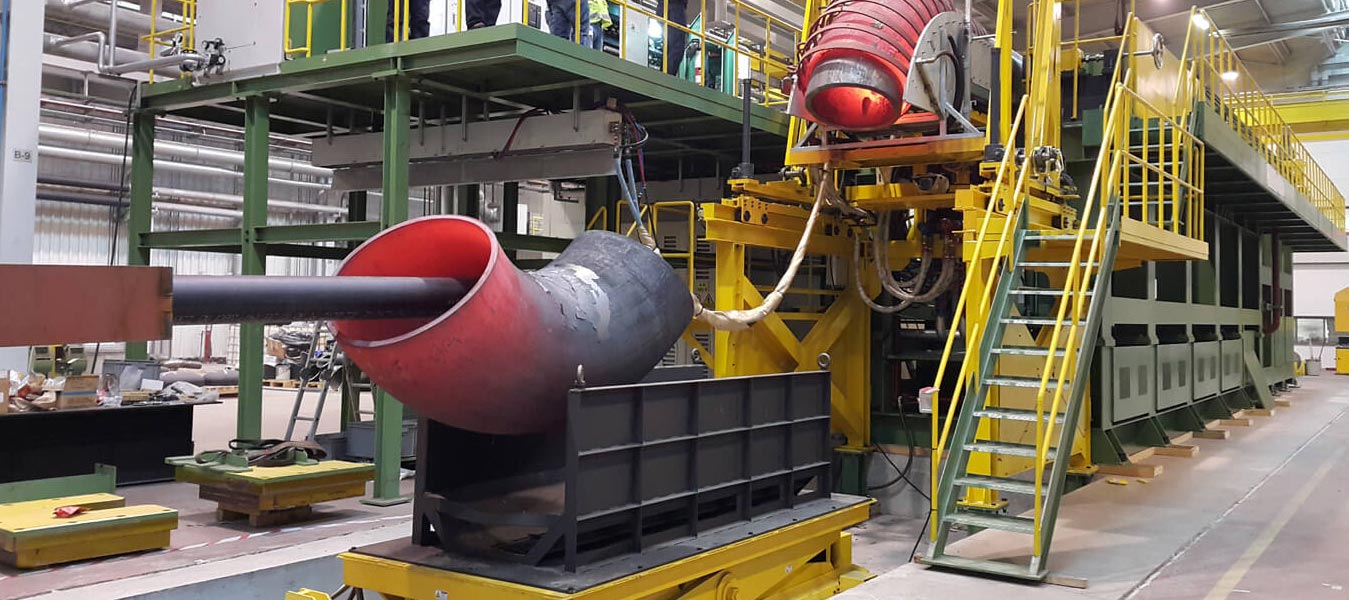
Induction Mandrel Pushing

Continuous medium-frequency induction heating ensures uniform thermal gradient along the pipe circumference, preventing wall thinning at outer extrados and ovality issues.

02
Computerized Normalizing

Controlled electric furnace heat treatment cycle (soaking at 900°C – 930°C followed by quiet still-air cooling) to eliminate residual forming stresses and homogenize ferrite-pearlite grain structure.

03
CNC Beveling & Facing

State-of-the-art CNC lathes machine bevel angles to 37.5° ± 2.5° or compound J-prep bevels per ASME B16.25, ensuring automated pipe aligners fit without grinding.

04
Full NDT & PMI Verification

Automated ultrasonic thickness gauging, wet fluorescent magnetic particle examination of high-stress crotches, and handheld XRF positive material identification prior to packing.

Inquire Now
Factory QA & Testing Protocol

Inside Rajtilak Metal's Factory Testing & Inspection Protocol

Take a transparent look at the stringent inspection regimes executed at our Mumbai manufacturing facility before ASTM A234 WPB components receive export clearance.

Spectrometric Chemical Verification

Direct-reading optical emission spectrometers (OES) verify ladle and product chemistry on every melt, ensuring strict compliance with carbon and phosphorus/sulfur ceilings.

Destructive Mechanical Testing

In-house 100-ton computerized tensile testing machines record true stress-strain curves, yield thresholds, elongation percentages, and Charpy impact energy absorbed at design temperatures.

Hydrostatic & NDT Non-Destructive Testing

100% radiographic inspection (RT) or phased array ultrasonic testing (PAUT) across all welded seam fittings (ASTM A234 WPBW), plus MPI testing on crotch transitions.

0
In-House Testing Laboratories
0%
Ultrasonic & PMI Verification
0%
Global Repeat EPC Clients
0%
Project On-Time Dispatch Rate
Integrity & Markings

Indelible Heat Number Stamping & EN 10204 3.1 Traceability

In high-pressure processing lines, counterfeit or downgraded materials cause fatal operational blowouts. At Rajtilak Metal, we enforce zero-compromise physical marking on every single ASTM A234 WPB fitting produced.

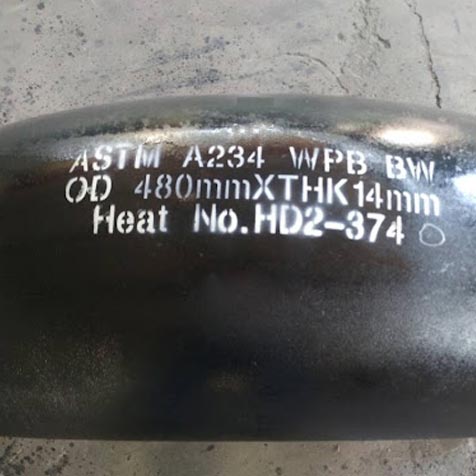
Every piece is marked along its circumference in accordance with MSS SP-25 and ASME B16.9 using low-stress dot-matrix computer stamps or vibro-etching: [Manufacturer Logo] - [Material Grade: ASTM A234 WPB] - [Fitting Type] - [Nominal Pipe Size] - [Wall Thickness/Schedule] - [Melt Heat Number]. This heat number corresponds uniquely to the EN 10204 3.1 inspection certificate provided in your shipping packet.

A
Melt Control

Prime parent pipes procured exclusively from Tier-1 mills.

B
Forming Verification

Extrados wall thickness calibrated via multi-point ultrasonic gauge.

C
Heat Treatment Log

Furnace time-temperature recorder charts logged per heat batch.

D
Preservation

Black rust-preventive varnish or rust-inhibitive primer dip coat.

Inquire Now
ASTM A234 WPB heat number and MSS SP-25 marking on buttweld elbow
Premier Manufacturer and Exporter of ASTM A234 WPB Pipe Fittings Since 1991
Enterprise Advantage

Why Global Energy Leaders Source ASTM A234 WPB Fittings from Rajtilak Metal

Metallurgical Engineering Excellence

Our metallurgy specialists review project specification datasheets, NACE MR0175 sour thresholds, HIC/SSCC testing parameters, and ASME Section IX weld procedures before production begins, preventing costly site rejections.

Integrated Piping Packages

One-stop supply capability: combine ASTM A234 WPB buttweld fittings with matching ASTM A105 forged flanges, ASTM A193 B7 stud bolts, and ASTM A194 2H heavy hex nuts packed together in seaworthy fumigated wooden crates.

Statutory & Global Certifications

Certified under ISO 9001:2015, recognized by the Government of India as an Export House, approved by Indian Boiler Regulations (IBR), and pre-cleared by major third-party inspection agencies including BV, DNV, SGS, TUV, and Lloyd's.

Headquartered in Mumbai, India, Rajtilak Metal maintains an extensive inventory of ready-to-ship ASTM A234 WPB seamless elbows, tees, and reducers from 1/2″ to 24″ in Standard, Schedule 40, Schedule 80, and Schedule 160 wall thicknesses. Exporting continuously across the Middle East (Saudi Arabia, UAE, Qatar, Oman), Southeast Asia (Singapore, Malaysia, Indonesia, Philippines), Europe, and North America.

Inquire Now
Complementary Components

Complete Carbon Steel Piping Systems: Matching Flanges & Fasteners

Save shipping transit time and procurement administration costs by bundling your ASME B16.9 buttweld fittings with precision-matched forged flanges and high-tensile pressure bolting.

AI & Buyer FAQs

Frequently Asked Questions Sourcing ASTM A234 WPB Pipe Fittings

Straightforward answers to the most common questions raised by procurement engineers, QA inspectors, and AI search inquiries regarding ASTM A234 Grade WPB components.

1. What does ASTM A234 WPB stand for, and what are its core mechanical minimums?

ASTM A234 is the standard specification covering wrought carbon steel and alloy steel piping fittings for moderate and high-temperature service. In the grade designation WPB: 'W' denotes Wrought/weldable, 'P' indicates Pressure service, and 'B' refers to the strength grade class. WPB corresponds directly to ASTM A106 Grade B pipe mechanical properties: a minimum yield strength of 35,000 psi (240 MPa) and a minimum tensile strength of 60,000 to 85,000 psi (415 to 585 MPa). It is suitable for design temperatures ranging from -29°C (-20°F) up to 427°C (800°F).

2. What is the fundamental difference between ASTM A234 WPB and ASTM A105?

While both materials represent carbon steels sharing virtually identical chemical compositions and mechanical strengths, the governing difference lies in product geometry and manufacturing standard. ASTM A234 WPB covers wrought buttweld fittings manufactured to ASME B16.9 and B16.28 (such as elbows, tees, reducers, and caps formed from pipe, plate, or forgings). Conversely, ASTM A105 covers forged carbon steel components intended primarily for ASME B16.5 flanges and ASME B16.11 small-bore forged socket weld and threaded fittings.

3. What is the difference between ASTM A234 WPB and ASTM A234 WPBW?

The suffix 'W' denotes welded construction. ASTM A234 WPB (without suffix) typically indicates a seamless fitting manufactured from seamless mother pipe. ASTM A234 WPBW designates a fitting manufactured from plate or ERW/EFW welded pipe that incorporates a fabrication weld seam. Per ASTM A234 specification rules, the weld seam on all WPBW fittings must undergo 100% radiographic (RT) or ultrasonic (UT) non-destructive examination across its entire length to verify weld joint efficiency.

4. Can ASTM A234 WPB fittings be certified for NACE MR0175 / ISO 15156 sour service?

Yes. Although base ASTM A234 WPB does not automatically meet sour service requirements, Rajtilak Metal regularly supplies WPB fittings with verified compliance to NACE MR0175 / ISO 15156. This requires three essential controls: (1) mandatory full normalizing heat treatment, (2) maximum Carbon Equivalent (CE) held under 0.43% with sulfur restricted below 0.005% for HIC resistance, and (3) hardness testing confirming parent material, weld metal, and heat-affected zone (HAZ) remain strictly at or below 22 HRC (250 HBW/HV).

5. What are the mandatory heat treatment requirements for hot-formed and cold-formed WPB fittings?

Per ASTM A234 section 7, hot-formed WPB fittings finished at temperatures above 1150°F (620°C) and cooled in still air do not mandate subsequent heat treatment if formed from normalized starting material. However, all cold-formed fittings where the outer fiber strain exceeds 5% must undergo stress-relieving, normalizing, or annealing. At Rajtilak Metal, all forged tees, heavy-wall reducers, and induction elbows undergo post-forming furnace normalizing at 910°C – 930°C to ensure optimum microstructure and stress relief.

6. How do I calculate the Carbon Equivalent (CE) for ASTM A234 WPB to ensure field weldability?

Carbon Equivalent is calculated per the International Institute of Welding (IIW) standard formula: CE = C + Mn/6 + (Cr + Mo + V)/5 + (Ni + Cu)/15. For problem-free automatic orbital and manual pipeline welding without preheat under typical ambient conditions, international pipeline specifications usually enforce CE ≤ 0.43% or CE ≤ 0.41% max. Every Rajtilak Metal EN 10204 3.1 MTC includes calculated CE values derived from actual ladle and product chemical analyses.

7. What third-party inspection (TPI) agencies can witness testing at your Mumbai works?

Our facility regularly hosts global third-party inspection agencies appointed by buyers or EPCs, including Bureau Veritas (BV), Lloyd's Register (LR), DNV GL, SGS, TÜV Rheinland, TÜV SÜD, Intertek, and Engineers India Limited (EIL). TPI scopes routinely include witness of ladle analysis, Charpy impact testing, tensile testing, 100% MPI on bevels, PMI verification, and visual-dimensional stamping audit.

Inquire Now
Operating Arenas

Deployments Across Mission-Critical Process Industries

From deep-sea production manifolds to refinery hydrocracker units, Rajtilak Metal ASTM A234 WPB buttweld fittings maintain global industrial fluids safely and continuously.

Upstream Oil & Gas
Refining & Petrochemicals
Offshore Platforms
Power & Steam Boilers
Chemical Processing
Water Utilities & Mining
Saudi ArabiaUnited Arab EmiratesQatarOmanKuwaitSingaporeMalaysiaIndonesiaPhilippinesUnited StatesUnited KingdomItalyPolandTurkeyEgypt

Ready for Direct Mill Pricing & Certified ASTM A234 WPB Supply?

Direct Engineering RFQ[email protected]