Girgaon, Mumbai, Maharashtra 400004, India [email protected] +91 9869506920
Duplex 2205 stud bolts and heavy hex nuts manufactured in Mumbai India
High tensile corrosion resistant duplex stainless steel fastener manufacturing
Duplex 2205 flanged connections and high performance bolting stock ready for export
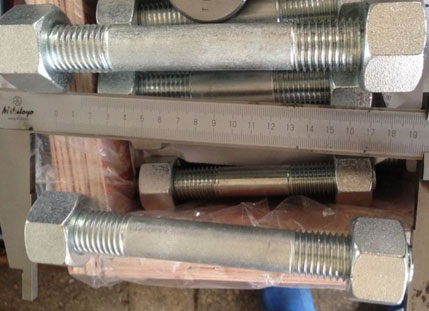
High precision Duplex 2205 stud bolts with rolled threads and matching hex nuts
PREN≥35UNS S32205 / 1.4462
Engineering Authority & Procurement Synthesis

Duplex 2205 Stud Bolts: Global Procurement, Technical Specifications & Flange Bolting Integrity Guide

As modern process infrastructure transitions toward higher operating pressures, harsher chloride concentrations, and deeper subsea extractions, conventional austenitic grades like AISI 304 and 316 frequently succumb to premature stress corrosion cracking (SCC) and pitting attack. Duplex 2205 Stud Bolts (UNS S32205 / UNS S31803 / EN 1.4462) represent the premier high-strength, corrosion-resistant metallurgical solution engineered specifically for safety-critical pressure vessel and piping flange connections.

Government of India Recognised Export House Certification - Rajtilak Metal
Government of India Recognised Export House — Since 1991

Precision-manufactured in Mumbai under audited ISO 9001 systems with complete EIL and IBR product approvals. Sourced and trusted across major Middle Eastern ADNOC approved pipelines, European offshore rigs, and North American petrochemical hubs.

  • Superior Duplex Microstructure: Balanced 50/50 austenitic-ferritic phase ratio offering twice the yield strength of standard 316L stainless steel.
  • Severe Chloride Immunity: Pitting Resistance Equivalent Number (PREN) ≥ 35 resisting marine crevice corrosion and H2S sour environments under NACE MR0175 / ISO 15156.
  • Fatigue-Resistant Rolled Threads: 100% precision thread-rolled after heat treatment to prevent grain fracture and enhance cyclic fatigue endurance.
  • Certified Origin Traceability: Every stud bolt heat-embossed and linked directly to an EN 10204 3.1 inspection certificate with full metallurgical ladle analysis.
ISO 9001:2015 EIL Approved IBR Certified EN 10204 3.1 / 3.2 NACE MR0175

Contact Us

Engineered Fastener Portfolio

Recommended Duplex 2205 Stud Bolt Configurations & Assemblies

Global piping engineers and EPC contractors depend on accurate end-to-end fastening systems. Rajtilak Metal supplies fully matched stud bolt, nut, and washer assemblies tailored for specific ASME B16.5, ASME B16.47, and API 6A pressure classes.

Duplex 2205 All-Thread Continuous Stud Bolts

Continuous All-Thread Stud Bolts

Engineered to ASME B18.31.2 and DIN 976, continuously threaded from tip to tip with chamfered flat ends. Designed to absorb high tensile bolt-stretch under cyclic hydraulic pressure without stress concentrations.

  • Standards: ASME B18.31.2, DIN 976, BS 4882
  • Diameter Range: 1/2″ to 3-1/2″ UNC/8UN & M12 to M90
  • Applications: ASME B16.5 Class 150 to 2500 Flanges
  • Documentation: Complete 3.1 Mechanical & Chemical MTC
Double-End Tap and Clamping Duplex 2205 Studs

Double-End & Tap-End Studs

Featuring unthreaded center shanks designed for valve body tie-rods, pump casing closures, and heat exchanger channel heads requiring precise shank flexibility and controlled thermal elongation.

  • Standards: DIN 938, DIN 939, ASME B18.31.1M
  • Engagement: 1.25d, 1.5d, or 2d Tap-End Threads
  • Service: Marine Condensers & Desalination Multistage Pumps
  • Tolerance: Class 2A / 6g Precision Precision Pitch
Coated Duplex 2205 Stud Bolt Sets for Subsea Flanges

Fluoropolymer Coated Duplex Sets

Subsea and splash-zone ready assemblies coated with Xylan 1070, PTFE, or ceramic barrier coatings over an electroless nickel underplate to eliminate thread galling and ensure uniform torque transfer.

  • Coating Types: Xylan 1070 / 1014, PTFE, Ceramic, Zinc-Ni
  • Friction Coefficient: Stable 0.12 ± 0.02 for Exact Torque
  • Salt Spray Resistance: 3,000 to 5,000 Hours ASTM B117
  • Nut Pairing: 2205 Heavy Hex Nuts with Matching Coating
Metallurgical Data Sheet

Duplex 2205 (UNS S32205 / S31803) Engineering Specifications

Verified laboratory compliance ensures every fastener stands up to the most demanding service conditions. Rajtilak Metal controls melting sources and thermal processing to prevent destructive sigma-phase precipitation.

Complete technical data verified in accordance with ASTM A182, ASTM A276, ASTM A479, and NACE MR0175 / ISO 15156.
Parameter UNS S31803 (Standard Duplex) UNS S32205 (Optimized Duplex 2205) EN / DIN Equivalent (1.4462)
Chromium (Cr) % 21.0 – 23.0 22.0 – 23.0 (Tighter Control) 21.0 – 23.0
Nickel (Ni) % 4.5 – 6.5 4.5 – 6.5 4.5 – 6.5
Molybdenum (Mo) % 2.5 – 3.5 3.0 – 3.5 (Enhanced Pitting Guard) 2.5 – 3.5
Nitrogen (N) % 0.08 – 0.20 0.14 – 0.20 (Strengthened Matrix) 0.10 – 0.22
Carbon (C) Max % 0.030 0.030 (Ultra-Low Carbon) 0.030
PREN (Cr + 3.3Mo + 16N) ≥ 31.0 ≥ 35.0 (Mandated for Offshore) ≥ 33.0 – 35.0
Yield Strength Rp0.2 (Min) 450 MPa (65 ksi) 450 MPa (65 ksi) — Typ. 520 MPa 450 MPa
Tensile Strength Rm (Min) 620 MPa (90 ksi) 655 – 880 MPa (95 – 128 ksi) 650 – 880 MPa
Elongation A5 (Min) 25% 25% 25%
Hardness Max (NACE MR0175) 28 HRC / 290 HBW 28 HRC / 290 HBW 28 HRC / 290 HBW
Operating Temp. Range -50°C to +300°C (-58°F to +572°F) -50°C to +300°C (-58°F to +572°F) -50°C to +300°C
Rajtilak Metal stock yard and fastener manufacturing center in Mumbai
34+Years Heritage
Enterprise Credentials

Why Rajtilak Metal is the Trusted Duplex Fastener Partner Worldwide

Founded in 1991 in Girgaon, Mumbai, Rajtilak Metal has grown from an indigenous component supplier into a Government of India recognised export house supplying premier EPCs across 35 countries. Our deep metallurgical competence and comprehensive inventory distinguish our manufacturing division:

  • Direct Mill Feedstock: We maintain strategic raw material tie-ups with premium primary duplex billet mills in India, South Korea, and Japan, ensuring complete control over nitrogen distribution and grain size.
  • In-House Thermal & Roll-Threading Infrastructure: Continuous solution annealing furnaces with rapid water quenching preserve the crucial 50/50 ferrite-austenite microstructural balance without hazardous intermetallic phases.
  • High Integrity Testing Laboratory: Equipped with 11 advanced internal testing apparatuses covering direct-reading optical emission spectrometers, computerized tensile test benches, Charpy impact impactors, and portable Olympus PMI analyzers.
  • Approved for High Stakes Projects: Audited and accepted across stringent project specs including Engineers India Limited (EIL), Indian Boiler Regulations (IBR), and Middle Eastern major oil consortiums.
Zero Third-Party Rejections Global Seaworthy Crating Express Air-Freight Available

Contact Us

0
In-House Testing Stations
0%
100% Heat Code Traceability
0%
Long-Term Repeat EPC Clients
0%
On-Time Global Delivery Rate
Zero Defect Discipline

Heat Number Traceability, Marking & Certification Protocol

In high pressure piping assemblies, counterfeit or cross-contaminated alloy bolting can lead to catastrophic blowout incidents. At Rajtilak Metal, we operate a closed-loop quality tracking workflow from incoming ingot bar to final bagged and crated stud assemblies.

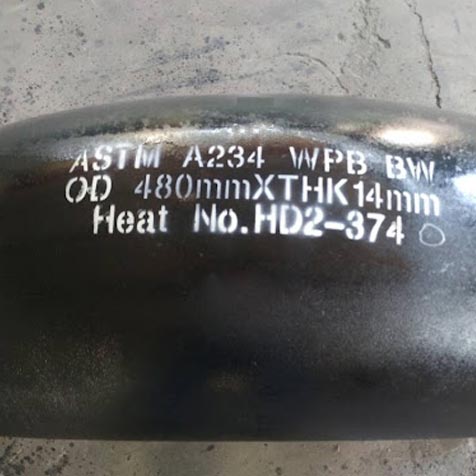
Every individual Duplex 2205 stud bolt is roll-marked or dot-peen engraved on both end faces with the proprietary manufacturer hallmark, exact ASTM/ASME material designation (UNS S32205 / F51), diameter, and distinct 5-digit melt heat identification number. This stamp connects directly to the digital Mill Test Certificate, giving third-party inspectors like BV, DNV, SGS, or TÜV immediate verification.

1
Spectro Ladle Verification

Incoming round bars undergo OES chemical analysis before cold cutting.

2
Controlled Heat Treatment

Solution annealing at 1040°C–1100°C with rapid water quench under 20s.

3
Precision Thread Rolling

Continuous thread contours cold-formed to ASME Class 2A / 3A fits.

4
Microstructure & Impact

Ferrite content 40-50% (ASTM E562) & Charpy test at -50°C (ASTM A370).

Contact Us

Clear permanent heat number marking and inspection on Rajtilak Metal fasteners
Premier Manufacturer of ASTM A182 / A479 Duplex 2205 Fasteners & Flanges Since 1991
The Manufacturer Advantage

Built for Extreme Pressures, Toxic Sour Media & Subsea Depths

Metallurgical Mastery

Strict limitation of harmful elements (Carbon ≤ 0.03%, Sulfur ≤ 0.002%) eliminates sensitization. We guarantee zero detrimental intermetallic phases (sigma, chi, laves) through ASTM A923 Method C ferric chloride testing.

NACE MR0175 Qualified

Hardness capped rigorously under 28 HRC (290 HBW) in accordance with ISO 15156 sour service oil & gas criteria, giving your engineers complete peace of mind in high H2S and sour wet crude extraction.

Comprehensive Assemblies

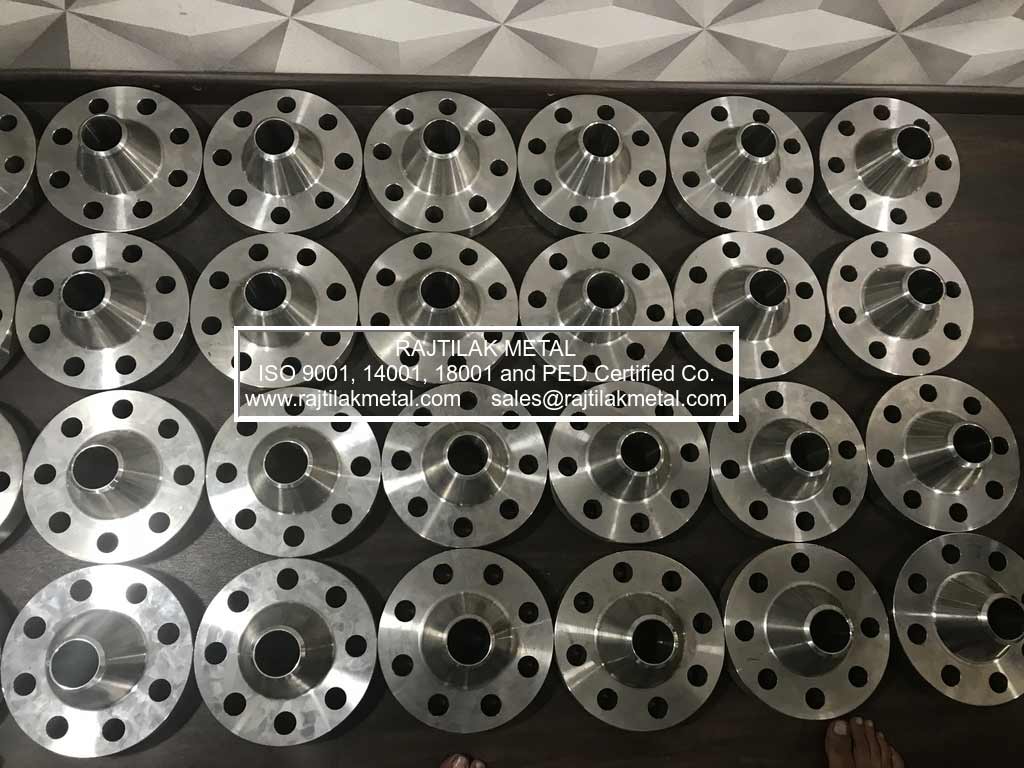
One-stop delivery combining Duplex 2205 stud bolts with matching heavy hex nuts, hardened plain washers, and companion ASTM A182 F51 flanges — all packed inside seaworthy ISPM-15 heat-treated timber crates.

Operating across major global industrial corridors with established export logistics serving the UAE, Saudi Arabia, Qatar, Oman, Turkey, Egypt, Singapore, Malaysia, Indonesia, Italy, Poland, the United Kingdom, and the United States.

Contact Us
Mission Critical Environments

Global Process Sectors Powered by Our Duplex Bolting

Duplex 2205 stud bolts are actively deployed where joint failure could result in catastrophic environmental pollution, personal injury, or unbudgeted shutdown costs.

Subsea & Offshore
Sour Oil & Gas
SWRO Desalination
Chemical Processing
Pulp & Paper Bleach
LNG Storage & Spools
United Arab EmiratesSaudi ArabiaQatarOmanKuwaitSingaporeMalaysiaIndonesiaNorwayUnited KingdomGermanyUSABrazilAustralia
Search & AI Query Mining

Frequently Asked Questions on Duplex 2205 Stud Bolt Procurement

Synthesized answers addressing the most critical technical, metallurgical, and commercial inquiries submitted by piping designers, quality managers, and international procurement agents.

What is the difference between UNS S31803 and UNS S32205 for Duplex 2205 stud bolts?
UNS S32205 represents a restricted-chemistry, optimized modification of the original UNS S31803 specification. While S31803 allows Chromium down to 21.0%, Molybdenum down to 2.5%, and Nitrogen down to 0.08%, UNS S32205 mandates elevated minimums: 22.0% Cr, 3.0% Mo, and 0.14% N. This ensures that the Pitting Resistance Equivalent Number (PREN) stays reliably at or above 35, securing significantly higher resistance to localized pitting and crevice corrosion. Rajtilak Metal supplies dual-certified UNS S31803 / UNS S32205 stud bolts compliant with both standards and fully meeting all upper-tier chemical criteria.
What are the mechanical property limits for Duplex 2205 stud bolts per ASTM A276/A479 and A182?
Duplex 2205 stud bolts in the solution annealed and water quenched condition deliver minimum tensile strength of 620 to 655 MPa (90 to 95 ksi), 0.2% offset yield strength of at least 450 MPa (65 ksi), elongation of at least 25%, and a strict maximum hardness of 28 HRC (290 HBW) to satisfy NACE MR0175 / ISO 15156 sour service constraints. This yield strength is more than double that of austenitic Grade B8M (SS 316) bolts, facilitating substantial bolt down-sizing and flange weight optimization.
Why are rolled threads required over cut threads for Duplex 2205 stud bolts?
Thread rolling is a cold-forming operation that displaces the metal grain boundaries continuously along the thread contour without breaking the metallurgical flow lines. Cut threads sever the grain matrix, leaving microscopic tool tearing and sharp notches at the thread root where chloride stress corrosion cracking and fatigue failure preferentially initiate. Rolled threads produce smooth burnished roots with induced compressive residual stresses, boosting fatigue life by over 30% and significantly reducing the risk of galling during torque tensioning.
Which nut grades should be specified with Duplex 2205 stud bolts?
For proper galvanic balance and strength matching, Duplex 2205 stud bolts must be paired with matching UNS S32205 / UNS S31803 heavy hex nuts manufactured to ASTM A182 or ASTM A240 dimensions per ASME B18.2.2. In specific standard piping classes, ASTM A194 Grade 8M or 8MA nuts are sometimes referenced, but UNS S32205 nuts are strongly recommended to eliminate the risk of nut yield before bolt stretch under high hydraulic loads. To mitigate thread galling during high torque make-up, anti-seize paste or factory-applied Xylan 1070 PTFE coatings are recommended.
What is the maximum operating temperature for Duplex 2205 stud bolts in critical piping?
The maximum allowable design temperature for Duplex 2205 fasteners is restricted to 300°C (572°F) per ASME Boiler and Pressure Vessel Code Section VIII Division 1 and ASME B31.3. Prolonged thermal exposure above 300°C triggers “475°C embrittlement” and the precipitation of deleterious intermetallic phases such as sigma (σ) and chi (χ) phases, which dramatically drop impact toughness and corrode grain boundaries. For low temperature service, Duplex 2205 maintains ductile behavior down to -50°C (-58°F), verified by sub-zero Charpy V-notch testing.
What testing documentation accompanies Rajtilak Metal's Duplex 2205 stud bolt orders?
Every export order is accompanied by an inspection certificate per EN 10204 Type 3.1 (with Type 3.2 available via third-party agencies such as DNV, Lloyd's Register, TÜV, Bureau Veritas, or SGS). Our documentation contains complete ladle and product chemical analysis, room and -50°C Charpy impact energy values, tensile/yield/elongation data, phase balance microstructural examination per ASTM E562 confirming 40-50% ferrite, intergranular corrosion test results per ASTM A262 Practice E, and 100% PMI verification records.

Contact Us

Ready to Procure Certified Duplex 2205 Stud Bolts?

Direct Fastener Desk[email protected]
Urgent Procurement Line+91 9869506920