

Engineered Alloy Steel Buttweld & Forged Fittings
Rajtilak Metal is an Indian manufacturer and global exporter of industrial alloy steel pipe fittings, chrome moly elbows, tees, reducers, stub ends, caps, and forged pressure connections. Engineered to excel in high-pressure thermal generation, steam headers, chemical reactors, and hydrogen refining service, our alloy steel fittings are produced from certified low-alloy and chromium-molybdenum steel stocks.
By precisely balancing Chromium (Cr) and Molybdenum (Mo), our alloy steel fittings provide exceptional high-temperature tensile strength, creep resistance, and resistance to hydrogen embrittlement. Every fitting undergoes stringent quality surveillance in accordance with ASME B16.9, ASME B16.11, MSS SP-75, and Indian Boiler Regulations (IBR).
- Full material compliance with ASTM A234 Grades WP1, WP5, WP9, WP11, WP22, WP91, and AISI 4130
- Seamless & welded buttweld fittings from 1/2″ through 48″ in Schedule 10 through Schedule XXS
- Computerized thermal normalizing, quenching, and tempering for verified mechanical strength
- 100% heat code stamping mapped to original steel mill melt certificates
Alloy Steel Buttweld & Forged Components
Manufactured under rigorous process controls for severe piping loops where standard carbon steel does not meet temperature or yield limits.
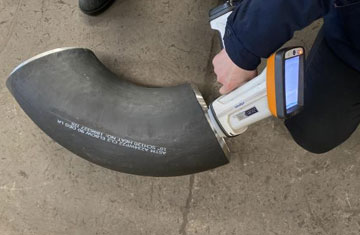
Alloy Steel 45° / 90° / 180° Elbows
Long radius (1.5D) and short radius (1.0D) seamless buttweld elbows with beveled ends to ASME B16.25.
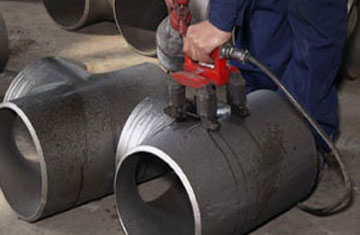
Equal & Reducing Tees
Uniform wall thickness and reinforced branch outlets for continuous fluid distribution without pressure dips.
Concentric & Eccentric Reducers
Precision-tapered transitions designed to manage fluid velocities and prevent cavitation in steam piping.
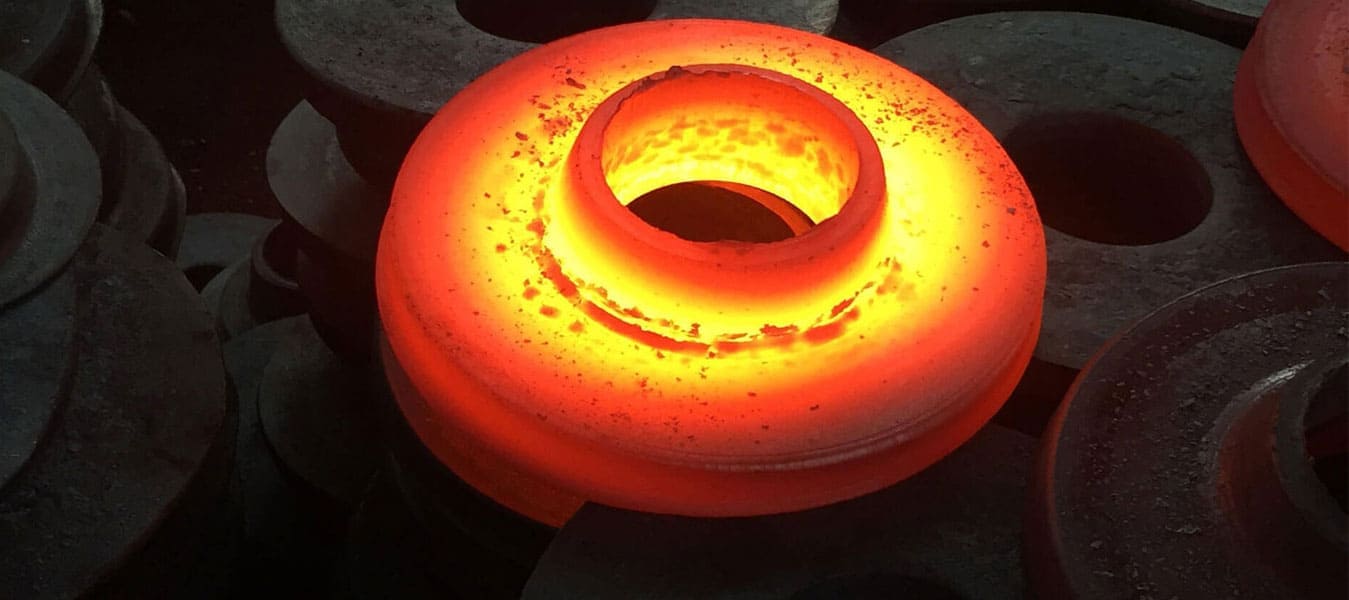
End Caps & Lap Joint Stub Ends
Dished elliptical pipe end closures and forged stub ends engineered for backing-flange assembly.
Standard Specification of Alloy Steel Pipe Fittings
Engineering parameters, pressure ratings, sizing range, and dimensional standards adhered to in our Mumbai production plant.
| Product Scope | Alloy Steel Pipe Fittings (Elbows, Tees, Reducers, Caps, Crosses, Bends, Stub Ends) |
| Manufacturing Standards | ASME B16.9, ASME B16.28, ASME B16.11, MSS SP-43, MSS SP-75, EN 10253-4, DIN 2605, JIS B2312, BS 1640 |
| Primary Material Grades | ASTM / ASME A/SA 234 WP1, WP5, WP9, WP11 (Class 1, 2, 3), WP12, WP22 (Class 1, 3), WP91, WP92, AISI 4130, 4140 |
| Connection Types | Buttweld (BW beveled per ASME B16.25), Socket Weld (SW per ASME B16.11), Threaded (NPT / BSPT) |
| Size Range | Seamless: 1/2″ NB to 24″ NB | Welded / Fabricated: 24″ NB to 48″ NB (Large diameters custom forged) |
| Wall Thickness / Schedules | SCH 5S, 10S, 20, 30, 40S, STD, 60, 80S, XS, 100, 120, 140, 160, XXS (Special non-standard thicknesses on request) |
| Pressure Rating | Classes 2000, 3000, 6000, 9000 for forged fittings; pipe-equivalent schedule ratings for buttweld components |
| Quality Certification | EN 10204 Type 3.1 MTC, IBR Form III-C certification, NACE MR0175 / ISO 15156 compliance upon request |
Alloy Steel Pipe Fittings Chemical Composition (%)
Strictly controlled chemistry ensures high yield strength, resistance to high-temperature scaling, and reliable weldability.
| Grade / Element | Carbon (C) | Manganese (Mn) | Phosphorus (P) | Sulfur (S) | Silicon (Si) | Chromium (Cr) | Molybdenum (Mo) | Vanadium (V) |
|---|---|---|---|---|---|---|---|---|
| ASTM A234 WP1 | 0.10 – 0.20 | 0.30 – 0.80 | 0.045 | 0.045 | 0.10 – 0.50 | — | 0.44 – 0.65 | — |
| ASTM A234 WP11 Cl.1 | 0.05 – 0.15 | 0.30 – 0.60 | 0.030 | 0.030 | 0.50 – 1.00 | 1.00 – 1.50 | 0.44 – 0.65 | — |
| ASTM A234 WP11 Cl.2/3 | 0.05 – 0.20 | 0.30 – 0.80 | 0.040 | 0.040 | 0.50 – 1.00 | 1.00 – 1.50 | 0.44 – 0.65 | — |
| ASTM A234 WP22 Cl.1 | 0.05 – 0.15 | 0.30 – 0.60 | 0.040 | 0.040 | 0.50 max | 1.90 – 2.60 | 0.87 – 1.13 | — |
| ASTM A234 WP22 Cl.3 | 0.05 – 0.15 | 0.30 – 0.60 | 0.040 | 0.040 | 0.50 max | 1.90 – 2.60 | 0.87 – 1.13 | — |
| ASTM A234 WP5 Cl.1/3 | 0.15 max | 0.30 – 0.60 | 0.040 | 0.030 | 0.50 max | 4.00 – 6.00 | 0.44 – 0.65 | — |
| ASTM A234 WP9 Cl.1/3 | 0.15 max | 0.30 – 0.60 | 0.030 | 0.030 | 0.25 – 1.00 | 8.00 – 10.00 | 0.90 – 1.10 | — |
| ASTM A234 WP91 | 0.08 – 0.12 | 0.30 – 0.60 | 0.020 | 0.010 | 0.20 – 0.50 | 8.00 – 9.50 | 0.85 – 1.05 | 0.18 – 0.25 |
Mechanical Properties of Low & High Alloy Steel Fittings
Verified through batch destructive mechanical testing, Charpy V-notch impact tests, and continuous hardness verifications.
| Material Grade | Tensile Strength min. ksi [MPa] | Yield Strength min. ksi [MPa] | Elongation in 2 in. (50mm) min. % | |
|---|---|---|---|---|
| Longitudinal | Transverse | |||
| ASTM A234 WP1 | 55 – 80 [380 – 550] | 30 [205] | 20 | 13 |
| ASTM A234 WP11 Class 1 | 60 [415] | 30 [205] | 22 | 14 |
| ASTM A234 WP11 Class 2 | 70 [485] | 40 [275] | 22 | 14 |
| ASTM A234 WP11 Class 3 | 75 [520] | 45 [310] | 22 | 14 |
| ASTM A234 WP22 Class 1 | 60 [415] | 30 [205] | 22 | 14 |
| ASTM A234 WP22 Class 3 | 75 [520] | 45 [310] | 22 | 14 |
| ASTM A234 WP5 Class 1 | 60 [415] | 30 [205] | 22 | 14 |
| ASTM A234 WP5 Class 3 | 75 [520] | 45 [310] | 22 | 14 |
| ASTM A234 WP9 Class 1 | 60 [415] | 30 [205] | 22 | 14 |
| ASTM A234 WP9 Class 3 | 75 [520] | 45 [310] | 22 | 14 |
| ASTM A234 WP91 | 90 [620] | 60 [415] | 20 | 13 |
ASME B16.9 Elbow Dimensions (Inches & Millimeters)
Engineering center-to-face reference standards for 90-degree and 45-degree long radius / short radius elbows.
| NPS | Outside Dia. (mm) | Outside Dia. (in) | 90° LR Center to Face | 90° SR Center to Face | 45° LR Center to Face | 180° Return Center to Center |
|---|---|---|---|---|---|---|
| 1/2″ | 21.3 | 0.840 | 1-1/2″ | — | 5/8″ | 2″ |
| 3/4″ | 26.7 | 1.050 | 1-1/8″ | — | 7/16″ | 2-1/4″ |
| 1″ | 33.4 | 1.315 | 1-1/2″ | 1″ | 7/8″ | 3″ |
| 1-1/2″ | 48.3 | 1.900 | 2-1/4″ | 1-1/2″ | 1-1/8″ | 4-1/2″ |
| 2″ | 60.3 | 2.375 | 3″ | 2″ | 1-3/8″ | 6″ |
| 3″ | 88.9 | 3.500 | 4-1/2″ | 3″ | 2″ | 9″ |
| 4″ | 114.3 | 4.500 | 6″ | 4″ | 2-1/2″ | 12″ |
| 6″ | 168.3 | 6.625 | 9″ | 6″ | 3-3/4″ | 18″ |
| 8″ | 219.1 | 8.625 | 12″ | 8″ | 5″ | 24″ |
| 10″ | 273.1 | 10.750 | 15″ | 10″ | 6-1/4″ | 30″ |
| 12″ | 323.9 | 12.750 | 18″ | 12″ | 7-1/2″ | 36″ |
Alloy Steel Buttweld Fittings Weight Chart (kg)
Theoretical shipping weights per piece across common schedules to assist freight estimation and structural support calculations.
| Nominal Size (DN) | Schedule 10S | Schedule 40S | Schedule 80S | ||||||
|---|---|---|---|---|---|---|---|---|---|
| 90° Elbow | 45° Elbow | Equal Tee | 90° Elbow | 45° Elbow | Equal Tee | 90° Elbow | 45° Elbow | Equal Tee | |
| DN 25 (1″) | 0.14 | 0.08 | 0.28 | 0.15 | 0.11 | 0.29 | 0.22 | 0.14 | 0.38 |
| DN 50 (2″) | 0.50 | 0.25 | 0.85 | 0.70 | 0.40 | 1.28 | 0.91 | 0.59 | 1.59 |
| DN 80 (3″) | 1.25 | 0.63 | 1.77 | 2.20 | 1.08 | 3.31 | 2.97 | 1.50 | 4.45 |
| DN 100 (4″) | 2.10 | 1.08 | 3.46 | 4.47 | 2.09 | 5.27 | 6.18 | 2.81 | 7.71 |
| DN 150 (6″) | 5.45 | 2.72 | 8.07 | 10.89 | 5.44 | 10.99 | 16.32 | 8.16 | 13.61 |
| DN 200 (8″) | 10.20 | 5.33 | 15.65 | 21.54 | 10.77 | 20.91 | 33.11 | 16.56 | 28.12 |
| DN 250 (10″) | 18.15 | 9.75 | 26.46 | 38.56 | 19.27 | 35.38 | 51.71 | 25.86 | 49.90 |
| DN 300 (12″) | 25.80 | 13.62 | 39.46 | 59.42 | 29.71 | 62.14 | 79.38 | 39.69 | 83.91 |
Allowable Working Pressures & Manufacturing Tolerances
Engineered to ensure zero leak paths under cycling thermal gradients and continuous hydrostatic head pressures.
Pressure-Temperature Ratings (psig)
| Temperature | Class 150 | Class 300 (1″) | Class 300 (2″) |
|---|---|---|---|
| -20°F to 150°F | 300 | 2000 | 1500 |
| 200°F | 265 | 1785 | 1350 |
| 300°F | 185 | 1360 | 1050 |
| 400°F | — | 935 | 750 |
| 500°F | — | 510 | 450 |
| 550°F | — | 300 | 300 |
ASME B16.9 Tolerances (mm)
| NPS | O.D. at Bevel | Wall Thickness (T) | Center-to-End |
|---|---|---|---|
| 1/2″ to 2-1/2″ | +1.6 / -0.8 | Not less than 87.5% of nominal thickness | ±1.6 |
| 3″ to 3-1/2″ | ±1.6 | ±1.6 | |
| 4″ | ±1.6 | ±1.6 | |
| 5″ to 8″ | ±1.6 | ±1.6 | |
| 10″ to 18″ | +4.0 / -3.2 | ±2.4 | ±2.4 |
Technical Questions Answered for Engineering Teams
What are the common ASTM material grades for alloy steel pipe fittings?
What heat treatment is applied to chrome-moly buttweld fittings?
Do you provide third-party inspection and EN 10204 3.1 inspection certification?
What non-destructive examination (NDE) methods are available for high-pressure fittings?
Request Certified Technical Quotations & Fast Track Delivery
Send your pipe fittings bill of materials, project line classes, and required NDT test criteria directly to our senior estimating engineers.
Contact Us