Manufactured to rigorous ASME, ASTM, DIN, JIS, and BS specifications under ISO 9001:2015, EIL, and IBR quality surveillance.
Founded & Manufacturing
In-House Testing Labs
Ultrasonic & PMI Verification
Global On-Time Export Rate
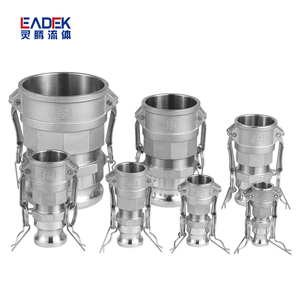
Socket weld fittings provide permanent, leak-tight connections for high-pressure, small-diameter piping lines (NPS 1/8 to NPS 4). Understanding critical dimensional tolerances and thermal expansion dynamics is vital for EPC engineering design.
Critical Engineering Principle (ASME B31.3 / B16.11): During the assembly of socket weld connections, an axial gap of approximately 1/16 inch (1.6 mm) must be maintained between the pipe end and the bottom shoulder of the socket fitting prior to welding. Failure to preserve this expansion gap leads to severe residual radial stresses during weld solidifying, often triggering crack propagation at the root of the fillet weld under thermal cyclic loading.
Unlike cast fittings or machined bar stocks prone to internal porosity, our custom OEM socket weld elbows, tees, couplings, and crosses undergo closed-die hot forging. This aligns grain boundaries directionally along component contours, guaranteeing fatigue resistance under high cyclic pulsation and intense hydrostatic shock.
Recognized by the Government of India as an approved Export House, our facilities carry certifications from Engineers India Limited (EIL) and Indian Boiler Regulations (IBR). Our components regularly serve tier-one Aramco, ADNOC, and QP projects across the GCC, backed by full EN 10204 3.1 mill test certificates.
Precision multi-axis CNC lathes machine the internal socket diameter, socket depth, bore diameter, and counterbore profile to stringent MSS SP-79 and ASME B16.11 tolerances. This ensures smooth flow velocity transitions without localized turbulence, cavitation, or erosive wear.
Correlating forged socket weld pressure designations with compatible wall thickness schedules for EPC pipeline stress calculations.
| Pressure Class Designation | Nominal Size Range (NPS) | Pipe Wall Equivalence | Standard Material Specifications | Design Temperature Scope |
|---|---|---|---|---|
| Class 3000 (3M) | 1/8″ to 4″ | Schedule 80 / Extra Strong (XS) | ASTM A105 Carbon Steel, A350 LF2 (Low Temp), A182 F304L/F316L | -46°C to +425°C |
| Class 6000 (6M) | 1/4″ to 2″ | Schedule 160 (SCH 160) | ASTM A182 F11, F22 (Chrome-Moly), Duplex UNS S31803 (F51) | -29°C to +593°C |
| Class 9000 (9M) | 1/2″ to 2″ | Double Extra Strong (XXS) | Super Duplex F53/F55, Inconel 625, Hastelloy C276, Monel 400 | Cryogenic to +650°C |
| MSS SP-79 Inserts | 1/4″ to 3″ | Variable Reduction Steps | ASTM A182 F316Ti, 904L, Titanium Grade 2 / Grade 5 | Corrosive Marine / Acid Duty |
Strategic structural shifts shaping how global procurement directors, engineering contractors, and supply chain managers source small-bore piping packages.
With accelerated capital expenditure in green hydrogen, ammonia, and CCUS (Carbon Capture, Utilization, and Storage), procurement protocols now mandate extreme helium leak tightness and micro-clean austenitic or high-nickel matrices (Inconel 625, 825) resistant to hydrogen embrittlement at 700+ bar pressure.
EPC clients increasingly reject paper-only documentation. The transition toward permanent 2D DataMatrix laser-etching on individual forged fittings enables immediate digital correlation with raw material ladle heat analysis, solution annealing furnace charts, and third-party witnessed EN 10204 3.2 certificates.
To reduce stocking complexity and minimize inventory risk, end-users prefer multi-certified alloys such as dual-grade 304/304L and 316/316L, alongside high-yield carbon steels conforming simultaneously to NACE MR0175 / ISO 15156 sour gas criteria with HIC (Hydrogen-Induced Cracking) test verification.
Global operators are de-risking single-source supply chains by establishing dedicated sourcing corridors with premier Indian manufacturers. With lower trade friction, proven open/closed die forging capabilities, and established logistics routes to the Middle East, Europe, and North America, Indian export houses are capturing primary vendor allocations.
Continuous investment in thermodynamic modeling, near-net shape forging, and non-destructive examination (NDE) technologies.
Modern field installation relies extensively on mechanised orbital TIG welding. We provide socket weld fittings with specialized pre-machined J-grooves, extended counterbore lands, and uniform outer body profiles that ensure repeatable weld pool heat dissipation and zero burn-through on thin-wall stainless process piping.
For abrasive slurry and high-pressure steam drop lines, we utilize finite volume CFD analysis to re-engineer internal fluid transitions within 90-degree elbows and reducing tees. Strategic fillet enlargement minimizes boundary-layer turbulence, cutting abrasive particle impact degradation by over 42%.
With LNG bunkering and cryogenic processing requiring extreme low-temperature ductility, our in-house metallurgical testing validates Charpy V-notch impact toughness at -196°C for austenitic stainless and special nickel alloy socket weld fittings, ensuring failure-proof performance in arctic and deepwater envelopes.
Clear, authoritative answers addressing technical specifications, inspection procedures, and international export logistics.
Whether you require standard ASME B16.11 Class 3000/6000 small-bore fittings or custom high-nickel alloy components manufactured to project drawings, our engineering team provides quotation and technical datasheet verification within 24 hours.