
Engineered Pipe Transitions, High-Integrity Forged Nipples, and Severe-Service Reducers Built to MSS SP-95 and ASME B16.11 for Gulf Coast Refineries, Midstream Terminals, and Subsea tie-ins.
Precision-manufactured swage nipples, forged flanges, and structural connection hardware available in ASTM A105, A350 LF2, A182 F316L, and High-Yield Chrome-Moly Alloys with complete mill certifications.
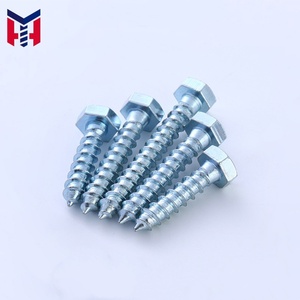
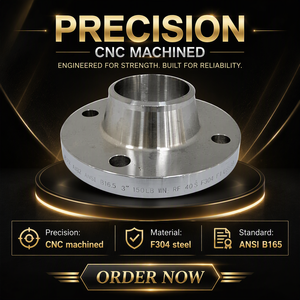
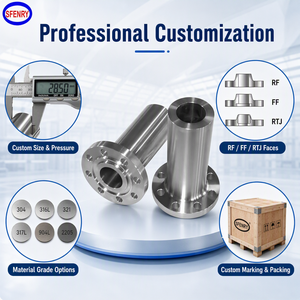
Unlike cast fittings or hand-turned piping stubs, high-performance swage nipples require thermo-mechanical forming, controlled grain alignment, and uniform wall preservation across transition bevels.
A swage nipple serves as the primary conduit transition between disparate pipeline diameters, typically bridging run piping to valves, relief manifolds, and pressure transmitters. In the rigorous chemical and refining complexes dotting the Houston Ship Channel, failure at a swage transition presents extreme runaway process safety hazards. Rajtilak Metal designs and manufactures swaged fittings from solid forgings and heavy-wall seamless pipe complying strictly with MSS SP-95, ASME B16.11, BS 3799, and API 6A specifications.
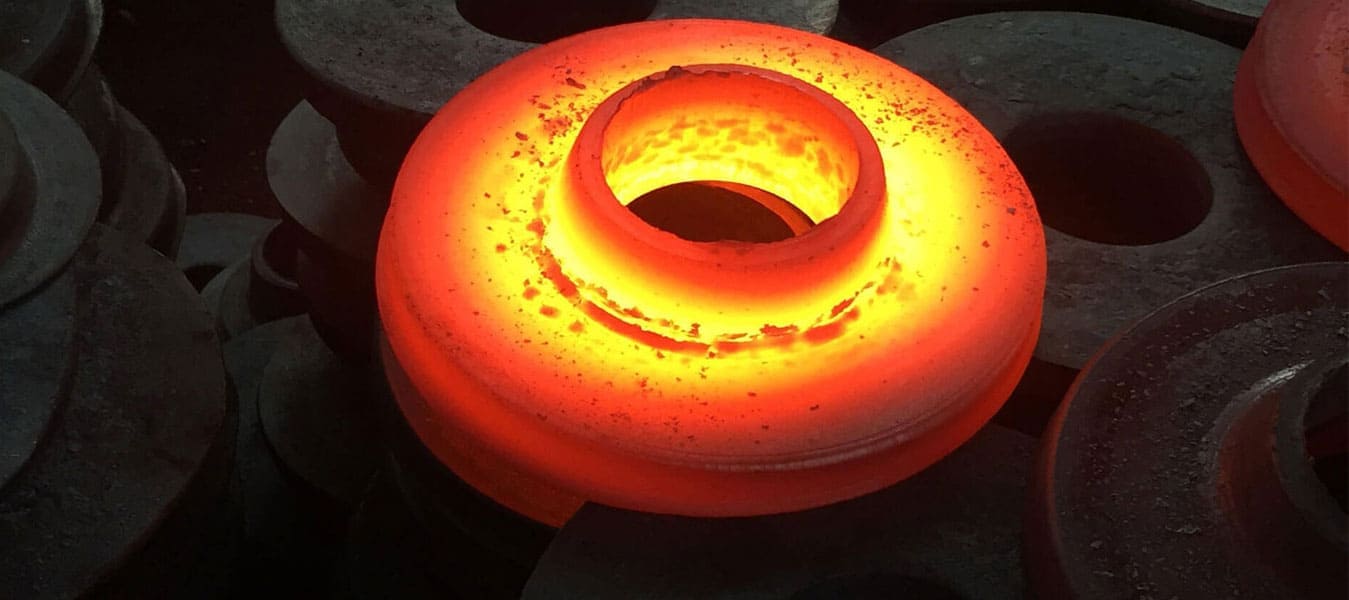
The manufacturing process begins with induction hot swaging or multi-station cold flow forming of raw billet stock or thick-walled pipe conforming to ASTM A105, A350 LF2 (for cryogenic arctic and LNG applications), or alloy grades like ASTM A182 F11, F22, and F91. Through accurate heating curves and progressive die forging, the internal crystalline fiber flow tracks the conical geometry of the reducer, eliminating laminar tearing, wall thinning, and non-metallic inclusion concentration along the reduction shoulder.

| Component Type | Dimensional Standard | Standard Materials | Size & Schedule Envelope | End Configurations |
|---|---|---|---|---|
| Concentric Swage Nipple | MSS SP-95 / BS 3799 | ASTM A105 / A106 Gr. B, A350 LF2, A182 F316/316L | 1/8″ NPS to 8″ NPS (Sch 40 up to XXS) | PBE, BBE, TBE, BLE/TSE, PLE/TSE |
| Eccentric Swage Nipple | MSS SP-95 / ASME B16.11 | ASTM A182 F11/F22, A403 WP304L/316L, Duplex 2205 | 1/4″ NPS to 6″ NPS (All Schedules) | BBE, TBE (NPT / BSPT / API Spec 5B) |
| Hexagonal Swage Nipple | MSS SP-95 / Factory Std | ASTM A105, 316 Stainless Steel, Monel 400 | 1/8″ NPS to 2″ NPS (Class 3000 / 6000) | Male NPT x Male NPT, Socket Weld End |
| Venting & Valve Nipples | MSS SP-95 / API 602 | ASTM A350 LF2 Class 1, ASTM A182 F51 / F53 | 1/2″ NPS to 2″ NPS (Sch 80 / 160 / XXS) | Beveled End x Threaded / Extended Male |
As the world's energy capital and a focal point for chemical manufacturing, the Houston industrial complex enforces distinct engineering mandates across refining, midstream, and LNG infrastructure.
Refineries along Baytown, Pasadena, and Texas City handle aggressive catalytic cracking and amine sweetening cycles. Our ASTM A182 F316L and A234 WP22 swage nipples operate continuously in fluid catalytic cracking units (FCCU) and hydrotreaters, where resistance to polythionic acid stress corrosion cracking (PASCC) and thermal cycling under high temperatures is paramount.
With the massive expansion of Gulf Coast LNG export terminals, piping systems require strict impact validation at cryogenic thresholds. Rajtilak Metal supplies Charpy V-Notch impact-tested ASTM A350 LF2 Class 1 and austenitic 304/304L swage reducers qualified down to -196°C (-320°F) to serve refrigeration liquefaction loops, boil-off gas compressors, and loading berths.
Crude gathering and fractionation infrastructure around Mont Belvieu process severe-service hydrocarbons containing wet H2S. Our MSS SP-95 swage nipples comply with NACE MR0175 / ISO 15156 standards, engineered with strict hardness limits (≤22 HRC) and minimal carbon equivalency (CE ≤ 0.42%) to protect pipeline manifolds from hydrogen-induced cracking (HIC).
Evaluating engineering, regulatory, and supply chain shifts redefining swage nipple and forged component procurement across Texas.
Houston's emergence as an official Clean Hydrogen Hub has mandated rigorous micro-crack and molecular containment protocols. Super-critical CO2 sequestration and high-pressure H2 lines utilize our high-grade stainless and alloy swages treated with electrolytic passivations and micro-polished internal bores to avert hydrogen embrittlement.
Houston EPCs (such as Bechtel, KBR, and Technip Energies) demand flawless traceability to mitigate counterfeit materials. Every Rajtilak Metal swage component is deep-stamped with unique Melt Heat Numbers directly reconciled to digital EN 10204 3.1 certification repositories accessible instantly via QR serialization.
With deepwater Gulf of Mexico tie-backs and sour chemical refining intensifying, standard carbon steel is steadily augmented by Duplex 2205, Super Duplex 2507, and Hastelloy C-276. We specialize in hot swaging these complex metallurgical alloys with precise post-weld solution annealing.
Over three decades of precision forging, government recognized export excellence, and rigorous compliance accreditations.
Founded in 1991, Rajtilak Metal has expanded from a dedicated regional forging plant in Mumbai into an internationally verified supplier recognized by the Government of India as an authorized Export House. We specialize in producing ASME B16.5, B16.9, B16.11, MSS SP-95, and EN 1092-1 compliant pipe fittings, forged flanges, and high tensile fasteners.
Our competitive advantage for the Houston market lies in end-to-end process control: from sourcing certified vacuum-degassed round bars and heavy-wall tubes from audited prime mills in South Korea, Japan, and India, to closed-die drop forging, high-speed CNC threading, and multi-point non-destructive testing (NDT).
Audited operational quality frameworks validating total adherence to dimensional tolerances, metallurgical grain patterns, and mechanical limits.
Uncompromised documentation dossiers accompanying every crate: complete chemical ladle, tensile, yield, elongation, and hardness test records.
Strict sulfur and phosphorus containment, controlled normalizing heat treatment, and verified hardness checks for sour gas service environments.
Accelerated maritime freight routes terminating directly at Port of Houston, Bayport, or George Bush Intercontinental Airport for critical emergencies.
Clear, direct answers regarding codes, lead times, NACE compliance, and non-destructive evaluations.