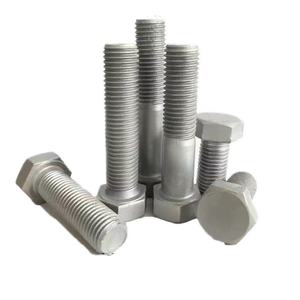

Direct-from-mill production, precision forging, CNC threading, and advanced anti-corrosion metallurgy designed to integrate into demanding European structural assemblies.
Civil and industrial foundations require absolute reliability against shear, tensile pull-out, cyclic seismic movement, and subsoil chemical exposure. We manufacture casting-in-place anchor bolts and post-installed anchoring systems rigorously tested according to EN 1992-4 (Eurocode 2 Part 4) and PN-EN 1993 (Eurocode 3).
Commonly referred to across Polish engineering drawings as śruby fundamentowe proste i fajkowe (DIN 529 / PN-82/M-82260 equivalents). Formed through hot bending and precision threading, ensuring zero internal micro-fractures in the knuckle section.
Fabricated anchor bolt cages equipped with bottom anchor plates (welded or double-nut secured), designed to redistribute dynamic uplift forces into deep concrete footings under heavy lateral wind shear.
For installations exposed to freeze-thaw salting cycles, coastal salinity, or chemical spills, we provide engineered surface protections designed to meet PN-EN ISO 10684 and PN-EN ISO 12944 classifications (C3 to CX marine corrosive levels).
Our manufacturing envelopes conform strictly to European testing methods. Review sizing, load parameters, and material alternatives below:
| Bolt Configuration | Reference Standards | Nominal Diameters | Material Class & Grades | Coating / Surface Protection |
|---|---|---|---|---|
| Bent Anchor Bolt (L & J Hook) | DIN 529, PN-82/M-82260, ISO 898-1 | M16 – M64 (5/8″ to 2-1/2″) | Class 4.6, 5.8, 8.8; S235JR / S355J2 | Plain, Zinc Electroplated, HDG (EN ISO 10684) |
| Stud Anchor with Plate Washer | ASTM F1554 Gr 36/55/105, EN 1993-1-8 | M20 – M72 (3/4″ to 3″) | Grade 8.8, 10.9; 42CrMo4, A193 B7 | Hot Dip Galvanized, Epoxy Coated, Sherardized |
| Pre-assembled Anchor Bolt Cage | Eurocode 2, Eurocode 3, Custom DWG | M24 – M100+ Complete Modules | High Tensile 8.8 & 10.9 Structural Steels | HDG Upper Exposed Threads + Bituminous Base |
| Coupled Foundation Tie Rods | DIN 6334, DIN 976, EN 10083 | M12 – M56 continuous / tapped | Stainless Steel 304/316, 1.4462 Duplex | Passivated, Pickled, Dacromet / Geomet |
| Severe Chemical Anchor Rods | ASTM A193 B8/B8M Class 2, EN ISO 3506 | M12 – M42 | SS 316L, 904L, Inconel 625, Hastelloy C276 | Self-passivating mill oxide / Micro-bead blasting |
Poland's strategic position as Central Europe's industrial, logistics, and emerging energy hub drives immense demand for rigorously verified structural fasteners.
Poland's massive Baltic Sea offshore wind program (near Łeba and Ustka) as well as inland wind projects across Pomerania and Wielkopolska require massive foundation anchor studs (M36-M72) able to resist severe fatigue, high cyclical oscillation, and salt fog corrosion according to EN ISO 12944-6 specifications.
The explosive expansion of logistics distribution parks along the A1, A2, and A4 motorways (Upper Silesia, Warsaw, Poznań, Wrocław) demands thousands of cast-in-place anchor bolts for structural precast concrete column footings, mezzanine floor supports, and high-bay racking anchorages.
Industrial refineries around Płock and Gdańsk, together with the Świnoujście LNG terminal expansion, require ASTM A193 B7/B8 structural tie bolts and heavy hex nuts paired with ASME B16.5 and EN 1092-1 forged components that maintain integrity under extreme pressures and cryogenic temperatures down to -196°C.
Understanding how European regulations, supply chain shifts, and sustainable energy transitions affect structural purchasing decisions in Central Europe.
Poland's Central Communication Port (Centralny Port Komunikacyjny - CPK) and the accompanying modernization of PKP Polskie Linie Kolejowe rail lines represent unprecedented capital investment. These mega-projects require foundation bolts and high-tensile fasteners certified under stringent European technical assessments (ETA) with zero material compromise.
Polish general contractors and structural fabricators are actively hedging risks by reducing over-reliance on unstable singular markets. Sourcing directly from reputable, ISO 9001 and IBR-approved Indian manufacturers with established sales representation in Poland guarantees price stability, swift shipping times, and fully verifiable material origin.
With massive public and private funds flowing into clean energy, including nuclear power planning and hydrogen transmission infrastructure, fastener specifications have shifted. Polish procurement teams now require low-alloy chrome-moly steels, high-yield fittings (WPHY), and corrosion-proof austenitic studs engineered for decades of zero maintenance.
Operating continuously since 1991, Rajtilak Metal combines deep metallurgical precision, international government recognitions, and targeted logistics serving Central Europe.
Accredited for cross-border engineering execution, handling complete customs documentation, EUR.1 preferences, and seamless DDP/CIF deliveries directly to your project sites across Poland.
Our quality management is audited to ISO 9001, Indian Boiler Regulations (IBR), and Engineers India Limited (EIL), ensuring all high-pressure and critical structural standards are exceeded.
Equipped with 11 in-house testing units conducting UTM tensile tests, Charpy V-notch impact tests at -196°C, hardness testing, PMI chemical verification, and hydrostatic testing.
From standard metric M12-M72 bolts to customized multi-ton forged anchor assemblies, non-standard lengths, matched heavy hex nuts (ASTM A194 2H / Class 10), and precision plate washers.
Direct answers to the most common inquiries raised by Polish project managers, procurement directors, and structural steel designers.
Yes. All anchor bolts, threaded studs, and heavy hex nuts can be manufactured to PN-EN ISO 898-1, DIN 529, EN 1993-1-8, or ASTM standards. We provide material properties that map directly to Eurocode 2 (concrete anchoring) and Eurocode 3 (steel connections) design calculations.
Every single shipment arrives with an authenticated EN 10204 3.1 Mill Test Certificate (MTC). The document details specific heat numbers, ladle chemical analysis, yield strength, ultimate tensile strength, elongation, reduction of area, impact test joules, and coating thickness.
We routinely coordinate third-party factory audits and lot witness testing with international inspection agencies nominated by our Polish clients, including TÜV Rheinland, SGS, Bureau Veritas, and DNV GL, prior to container stuffing and dispatch.
Sea freight shipments are shipped directly from Nhava Sheva (Mumbai) to the Ports of Gdańsk or Gdynia with typical maritime transit times of 28 to 35 days. For time-sensitive emergency plant shutdowns or immediate milestone deliverables, express air freight to Warsaw Chopin (WAW) or Katowice (KTW) is available.
Yes. We operate extensive open-die forging, cold heading, and CNC machining facilities. We fabricate complete foundation kits based on DXF/DWG/PDF engineering specifications, including welded base plates, shear tabs, PVC sleeves, and matched double locking nuts.
Our hot-dip galvanizing process complies fully with PN-EN ISO 10684 and ASTM A153. Threads are precision-machined or undercut where necessary according to ISO tolerance classes (6g/6H or 6AZ/6AX) to guarantee smooth engagement without flaking or binding on site.
Consult with our structural metallurgists and export engineering desk. Receive an itemized technical offer, dimension sheet confirmation, and competitive FOB/CIF Poland quotation within 24 hours.