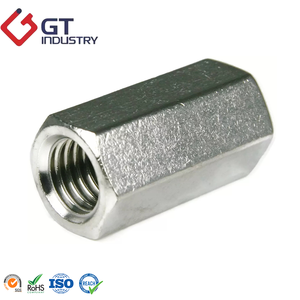
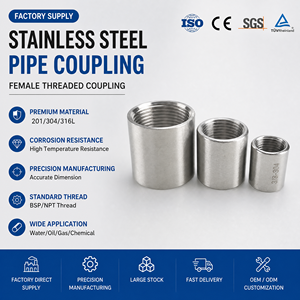
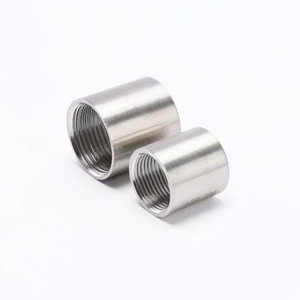
In modern high-pressure piping assemblies, chemical processing lines, and fluid logistics infrastructure, the mechanical integrity of threaded couplings dictates total system reliability. As an engineering-driven China threaded coupling manufacturer and global export house, we combine computer-numerical-controlled (CNC) multi-axis machining with stringent metallurgical quality systems. Our manufacturing scope encompasses full couplings, half couplings, reducing sockets, camlock adapters, and heavy-duty hex coupler nuts engineered to withstand thermal cycling, aggressive hydraulic hammer, and corrosive media.
Whether your fluid circuit calls for ASME B16.11 Class 3000 / 6000 forged fittings, ISO 228-1 parallel BSPP interfaces, or ANSI/ASME B1.20.1 NPT taper seals, each manufactured lot delivers 100% thread profile compliance, verified through Go/No-Go calibrated thread gauges, optical profilometry, and EN 10204 3.1 chemical and mechanical traceability back to prime molten heats.
Engineered for petroleum processing, fluid logistics, pharmaceutical synthesis, and industrial engineering applications. Fully customizable by dimension, pressure envelope, and thread geometry.
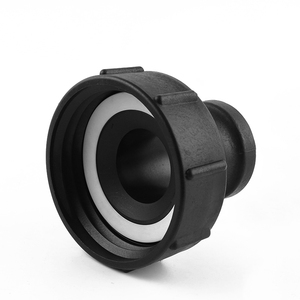
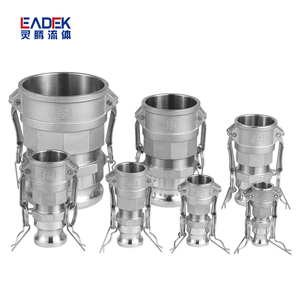
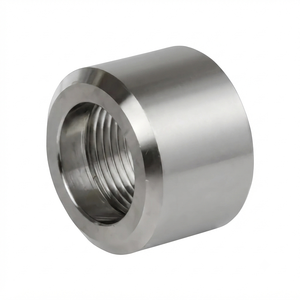
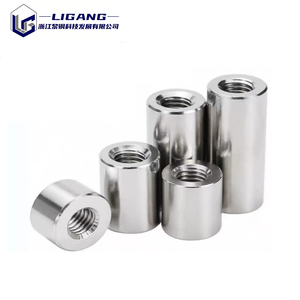
Comprehensive metallurgical grades, pressure classes, and dimensional parameters for industrial piping engineers.
| Coupling Class | Governing Standard | Nominal Size Range | Rating / Wall Schedule | Primary Alloy Options | Thread Profiles |
|---|---|---|---|---|---|
| Forged Full Coupling | ASME B16.11 / BS 3799 | 1/8" to 4" (DN6 – DN100) | Class 2000, 3000, 6000, 9000 | ASTM A105, A182 F304/304L, F316/316L, A350 LF2 | NPT / ASME B1.20.1 |
| Forged Half Coupling | ASME B16.11 / MSS SP-83 | 1/8" to 4" (DN6 – DN100) | Class 3000, 6000 (Sch 80 / Sch 160) | A182 F316L, F321, F51 Duplex 2205, Inconel 625 | NPT / BSPT / RC |
| Light Industrial Couplings | ISO 4144 / MSS SP-114 | 1/8" to 6" (DN6 – DN150) | 150 LB / PN16 / PN25 | Investment Cast CF8 (304), CF8M (316) | ISO 7-1 (BSPT) / ISO 228 (G) |
| Hex Long Coupler Nuts | DIN 6334 / IFI 128 | M6 to M48 (1/4" to 2" UNC) | Tensile Class 50, 70, 80 / Gr. 8.8 | A2-70, A4-80, Carbon Steel Zinc / HDG Plated | Metric 6H / UNC Class 2B |
| Quick-Camlock Couplings | A-A-59326 / EN 14420-7 | 1/2" to 8" (DN15 – DN200) | 100 PSI – 250 PSI (Hydrotested) | ASTM A351 CF8M, Aluminum A356, Brass, POM | NPT / BSPP Flat Face Gasket |
| Sanitary Hybrid Couplings | 3-A Sanitary / DIN 11851 | 1/2" to 4" (OD Tube sizes) | 150 PSI (Sanitary Clamp Clamping) | AISI 316L (Forged bar, Sulfur 0.005-0.017%) | NPT Female to Sanitary Clamp |
A frequent root cause of pipeline leakage in processing plants is the improper pairing of taper and parallel thread standards. Understanding thread geometry is critical during coupling procurement:
Correct selection between coupling configurations determines hydraulic efficiency and fabrication speed:
How global supply chain volatility, decarbonization regulations, and automated inspection are reshaping B2B industrial coupling procurement.
Purchasers are shifting from upfront unit cost comparisons toward Total Cost of Ownership (TCO). Inconsistent thread depths from unvetted workshops cause job-site cross-threading, galling, and hydrotest blowout failures. Tier-1 buyers increasingly mandate single-source China manufacturers that provide certified steel melts with strict sulfur and carbon controls.
100% Raw Heat TraceabilityThe transition to digitized cloud-verifiable documentation is accelerating. Project engineers require QR-coded optical markings directly on coupling bodies linking directly to chemical spectrometry, yield strength, tensile elongation, and Charpy V-Notch impact test values to comply with ASME Sec VIII and PED 2014/68/EU directives.
Tamper-Proof Digital MTCTo reduce freight emissions and customs handling charges, EPC procurement leaders are abandoning piecemeal ordering. Threaded couplings are increasingly bundled together with forged flanges, socket weld fittings, and ASTM A193/A194 stud fasteners into single, seaworthy container shipments categorized by spool isometric drawings.
Unified Modular PackagingPioneering advancements in automated manufacturing lines, metallurgy, and anti-corrosion barrier coatings.
Traditional single-point lathe cutting is being replaced by high-speed CNC thread whirling. This process eliminates burrs, optimizes chip evacuation, and maintains surface roughness tolerances below Ra 0.8μm, minimizing thread flank micro-imperfections.
With offshore subsea and seawater desalination projects operating under severe chloride stress corrosion cracking environments, couplings forged in Duplex 2205 (S31803), Super Duplex 2507 (S32750), and 6-Moly alloys (254SMO) are replacing conventional 316L.
The green hydrogen economy demands couplings with virtually zero molecular micro-porosity. Forged bar stock undergoes specialized vacuum degassing and ultrasonic non-destructive testing (NDT) to prevent hydrogen embrittlement across critical high-pressure joints.
Moving beyond manual thread plug gauges, automated optical sensors scan 100% of thread root depths, pitch diameters, and lead angles in real-time on our CNC cells, automatically ejecting parts showing deviations greater than ±0.005mm.
Combining three decades of precision metallurgy with large-scale production capacity and international certifications.
Operating under accredited ISO 9001:2015, ISO 14001, and CE PED quality management frameworks. Our threaded couplings and high-pressure fittings are pre-approved for major industrial projects across the Middle East, Southeast Asia, Europe, and the Americas.
PED 2014/68/EU • AD2000-W0We maintain an active reserve of over 2,500 metric tons of certified stainless steel (304/304L, 316/316L), carbon steel (A105, A350 LF2), and alloy steel billets and coupling blanks, ensuring standard size orders dispatch within 48 to 72 hours of verification.
Rapid 72-Hour Dispatch BufferEquipped with Swiss-type multi-axis CNC lathes, cold-heading stations, and automated broaching centers, we readily produce non-standard coupling geometries, custom wall schedules, hybrid threads (e.g., metric to NPT conversion), and high-pressure hydraulic blocks.
CAD/CAM In-House ToolingStraightforward technical answers regarding sizing, standards, metallurgy, and shipping terms.
Class ratings (designated under ASME B16.11) reflect cold working pressure envelopes rather than literal maximum PSI at high temperatures. A Class 3000 threaded full coupling is designed to match the nominal pressure rating of Schedule 80 or Schedule 160 seamless pipe, while Class 6000 couplings match Schedule XXS pipe wall thickness. Class 6000 fittings possess significantly larger outside diameters (OD) and heavier wall cross-sections to resist hoop stresses during severe pressure spikes and thermal transients.
No. Although both NPT and BSPT share a 1:16 taper ratio, their thread forms are incompatible. NPT utilizes a 60-degree flank angle with flattened peaks and valleys (crests/roots), whereas BSPT (Whitworth / ISO 7-1) features a 55-degree flank angle with rounded crests and roots. In addition, the pitch (threads per inch) differs across key nominal sizes (such as 1/2" and 3/4"). Forcing an NPT fitting into a BSPT coupling will result in thread cross-binding, galling, and high-pressure fluid leakage.
Austenitic stainless steels (SS304, SS316, 316L) form an instantaneous chromium oxide passive layer. During mechanical torque makeup, friction breaks this film, causing bare metal crystals to fuse and seize (galling). We prevent this through: (1) Superior surface finish via thread whirling with Ra < 0.8μm; (2) Controlled mechanical clearances matching Class 2B/6H gauges; and (3) Factory-applied surface treatments upon request, including silver electroplating, Kolsterising surface hardening, or specialized molybdenum disulphide dry-film lubricants.
Every commercial container shipment is dispatched with an EN 10204 3.1 Inspection Certificate documenting actual chemical ladle analysis (Carbon, Silicon, Manganese, Phosphorus, Sulfur, Chromium, Nickel, Molybdenum) and mechanical test results (tensile strength, yield point, elongation percentage, and Brinell/Rockwell hardness). Each coupling is physically roll-stamped or laser-engraved with heat number, nominal size, pressure class, material grade, and trademark for 100% field traceability.
Yes. We regularly coordinate inspections with recognized international third-party agencies including SGS, Bureau Veritas (BV), TÜV SÜD, DNV-GL, and Lloyd's Register. TPI inspectors typically witness dimensional verification, Go/No-Go thread gauging, hydrostatic pressure holding tests, Positive Material Identification (PMI) by portable XRF spectrometer, and review packaging compliance with international seaworthy standards (fumigated wooden crates, thread end protectors).
For custom non-standard geometries or special alloys (such as Alloy 20, Hastelloy C-276, Monel 400, or customized hybrid-thread couplings), initial engineering drawing review and tooling setups take 3 to 5 business days. Pilot sample verification requires 7 to 10 days, followed by commercial mass-run production completed within 20 to 30 days depending on raw billet procurement cycles and order volume.
Send your pipe coupling datasheets, 2D/3D part drawings, or project bills of quantities (BOQ). We will review thread tolerances, verify metallurgical grades, and deliver a comprehensive commercial quotation with Mill Test Certifications within 12 hours.