Precision engineered pipe fittings, forged flanges, and high-pressure threaded components manufactured under ISO 9001 and verified through EN 10204 3.1 certification.
Get instantaneous access to dimensional tolerances, pressure-temperature ratings, and raw forging certifications tailored for Uzbek industrial import regulations.
ASME B16.11 governs forged fittings, socket-welding, and threaded systems engineered to handle small-bore process fluids (DN6 to DN100 / 1/8" to 4") where welded joints are either impractical or maintenance require non-destructive disassembly.
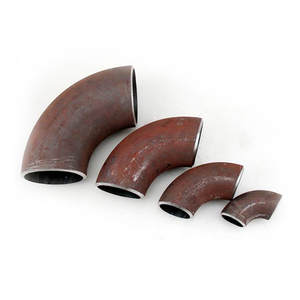
Threaded 90-degree and 45-degree elbows forged to ASME B16.11 provide substantial mechanical superiority over conventional casting processes. During closed-die forging, continuous grain flow conforms strictly to the angular curvature of the elbow wall, effectively eliminating internal porosity, hot tears, and dendritic segregation typical of cast products. Under pulsating pressure regimes common in reciprocating gas compressors or high-pressure bypass lines, directional grain refinement delivers superior Charpy V-notch impact toughness and enhanced resistance to fatigue cracking.
Rajtilak Metal manufactures ASME B16.11 threaded elbows strictly from normalized ASTM A105 forged carbon steel, sub-zero impact-tested ASTM A350 LF2 (Classes 1 and 2), austenitic stainless steels (ASTM A182 F304/F304L, F316/F316L, 904L), and high-temperature chrome-moly alloys (ASTM A182 F11, F22). For sour service installations, full compliance with NACE MR0175 / ISO 15156 is maintained through precise control of carbon equivalents (CE ≤ 0.42%) and automated post-weld/forging heat treatment, limiting hardness beneath 22 HRC to arrest sulfide stress cracking (SSC).
Our OEM/ODM thread execution adheres to strict optical and mechanical gauging procedures. The standard American National Standard Taper Pipe Thread (NPT) utilizes a 1-in-16 taper ratio (3/4 inch per foot) on diameter. Each thread profile is CNC-single-point cut rather than tapped where maximum concentricity is specified. This avoids microscopic tear marks that cause galling or leak paths under high-pressure gas testing.
Each production batch undergoes L1 (hand-tight engagement gauge), L2 (effective thread length gauge), and crest-to-root truncation checks with optical profile comparators, ensuring gas-tight sealing when paired with anaerobic paste or PTFE tape sealants.
| Nominal Pipe Size (NPS) | Class 2000 Rating (C-to-E 90°) | Class 3000 Rating (C-to-E 90°) | Class 6000 Rating (C-to-E 90°) | Min. Wall Thickness (Class 3000) | Primary Material Grades |
|---|---|---|---|---|---|
| 1/4" (DN 8) | 21 mm | 25 mm | 29 mm | 3.30 mm | ASTM A105 / A182 F316L / LF2 |
| 1/2" (DN 15) | 25 mm | 33 mm | 38 mm | 4.09 mm | A105 / A350 LF2 / F304L |
| 3/4" (DN 20) | 29 mm | 38 mm | 44 mm | 4.32 mm | A105 / A182 F11 / F316L |
| 1" (DN 25) | 33 mm | 44 mm | 51 mm | 4.98 mm | ASTM A105 / A350 LF2 Cl.1 |
| 1-1/2" (DN 40) | 44 mm | 60 mm | 64 mm | 6.05 mm | A182 F316L / Duplex 2205 |
| 2" (DN 50) | 51 mm | 64 mm | 84 mm | 6.98 mm | ASTM A105 / A350 LF2 / F22 |
Uzbekistan represents the industrial and petrochemical epicenter of Central Asia. The deployment of ASME B16.11 threaded elbows encounters distinct operational, climatic, and metallurgical challenges across the republic's primary production nodes.
The Shurtan Gas Chemical Complex and the landmark Oltin Yo'l GTL (Gas-to-Liquids) installation in Kashkadarya process high-pressure hydrocarbons characterized by significant H2S, CO2, and wet condensates. ASME B16.11 Class 3000 and Class 6000 90° elbows are extensively specified on skid-mounted sampling manifolds, pneumatic safety shutdown loops, and chemical injection quills. In these critical loops, A182 F316L and NACE-certified A350 LF2 elbows safeguard against severe localized pitting and hydrogen-induced cracking (HIC).
Undergoing multi-stage modernization to yield Euro-5 standard gasoline and clean diesel, the Bukhara and Fergana refineries require ASME B16.11 chrome-moly threaded elbows (ASTM A182 F11 and F22) for catalytic cracking units, hydrogen reformators, and steam utility piping. Class 6000 NPT elbows handle high-temperature hydrogen service up to 550°C where microstructural resistance against hydrogen attack (Nelson curve compliance) is non-negotiable.
The Almalyk Mining and Metallurgical Complex (AMMC) and Navoi Mining and Metallurgical Complex (NMMC) operate deep extraction and hydrometallurgical processing circuits for copper, gold, and uranium. Small-bore leaching pipes carrying sulfuric acid slurries depend on Class 3000 threaded elbows forged from 904L, Alloy 20, or Duplex 2205 stainless steels to resist extreme erosive-corrosive combinations and high vibrations caused by positive displacement dosing pumps.
Pipeline compressor stations along the Central Asia-China Gas Pipeline and Ustyurt gas processing facilities endure continental climate extremes ranging from -35°C in sub-zero winter blizzards to +50°C in desert summers. We export ASTM A350 LF2 Class 1 low-temperature forged elbows tested at -46°C (Charpy V-notch values exceeding 27 Joules minimum average). This prevents catastrophic ductile-to-brittle transition failures common in standard carbon steels under unexpected pressure spikes during arctic-type winter freeze-overs.
Uzbekistan is aggressively transitioning from a raw natural gas exporter to a regional hub for high-value polymers, downstream chemicals, and modern power generation under its National Development Strategy.
International consortium investments in Uzbek energy infrastructure (involving EPCs from Europe, China, Korea, and the Gulf) have expedited the transition from legacy Soviet GOST standards (GOST 17375, GOST 8966) toward ASME B16.11 and ASME B31.3. Threaded elbows manufactured to precise ANSI/ASME dimensions eliminate mismatch errors on skid modules pre-fabricated abroad.
The development of the MTO (Methanol-to-Olefins) gas chemical complex near Karakul and new polyethylene/polypropylene trains at Shurtan require thousands of high-pressure small-bore piping connections. The preference is firmly shifting toward Class 3000 and Class 6000 forged threaded elbows that facilitate rapid installation and zero hot-work permitting in explosive hazardous zones.
Pilot green hydrogen ventures in Chirchiq and carbon capture initiatives tied to thermal power plants require specialized threaded components with strict helium-leak and gaseous diffusion tightness. Super austenitic alloys and high-purity ASTM A182 F316L threaded elbows prevent micro-leakage in dry hydrogen distribution panels operating at up to 400 bar.
Uzbekistan’s landlocked geography has stimulated optimized supply chains utilizing the International North-South Transport Corridor (INSTC) and Caspian maritime transit. Rajtilak Metal leverages direct multimodal rail and container routes from Mumbai to Bandar Abbas, onward via Sarakhs/Turkmenistan directly to Tashkent Customs Terminal, shortening lead times down to 18-24 days.
Founded in 1991 in Mumbai, India, Rajtilak Metal has grown into a Government of India Recognised Export House, recognized globally for forged pipe fittings, precision flanges, and high-tensile fasteners.
Rajtilak Metal is an ISO 9001 certified company holding prestigious Indian Boiler Regulations (IBR) approval and Engineers India Limited (EIL) qualifications. We possess substantial track record supplying critical-service components for major international project frameworks, including ADNOC-approved installations across the Middle East and Central Asian EPC developments.
Our quality laboratory houses 11 specialized testing rigs including in-house Positive Material Identification (PMI via XRF and OES spectrometers), Charpy impact test equipment capable of sub-zero cryogenic testing down to -196°C, Brinell/Rockwell hardness testers, tensile machines, and hydrostatic test manifolds capable of verifying threaded fitting bodies up to 15,000 PSI.
Every single ASME B16.11 threaded elbow shipped to Uzbekistan is permanently stamped with manufacturer insignia, size, class rating, material grade, and unique melt heat number, directly referenced against an EN 10204 3.1 Mill Test Certificate containing complete chemical melt analyses and mechanical property verification.
Addressing common cross-border procurement challenges regarding ASME standardization, customs clearance, and delivery across Uzbekistan.
Direct factory quotations, comprehensive stock availability, and tailored logistical documentation for EPC contractors across Uzbekistan.