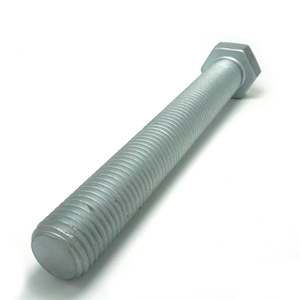
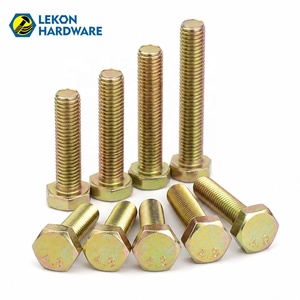
Galvanized DIN933 M4-M24 Grade 8.8 Hex Bolts
High-tensile zinc plated and plain carbon steel bolting designed for Hungarian roof, facade, and industrial door frames.

Explore our integrated production line tailored for extreme mechanical loading, thermal cycling, and EN 10204 3.1 material traceability demands across Central Europe.
Why modern Central European civil, chemical, and energy projects specify cold-forged and hot-headed heavy hex nuts over standard commercial metric hardware.
Heavy Hex Nuts (ASME B18.2.2, EN 14399-4) possess significantly larger 'width across flats' (WAF) compared to standard ISO 4032 fasteners. This dimensional enhancement distributes massive clamping preloads over a broader contact surface, substantially mitigating localized flange embedment and preventing premature torque relaxation under cyclic micro-vibrations.
Our ASTM A194 Grade 2H and Grade 7 heavy hex nuts undergo continuous-line induction hardening followed by secondary tempering. This metallurgical process guarantees strict core hardness limits (24 to 35 HRC) while eliminating micro-cracking and notch brittleness, ensuring guaranteed proof-load ratings exceeding 175,000 psi (1,205 MPa).
CNC-tapped 2B and 6H internal thread tolerances are calibrated with micro-honed entry chamfers. When mated with high-tensile studs or A193 B7 bolts, our nuts ensure frictionless engagement without thread strip. For stainless A194 Gr 8/8M alloys, specialized molybdenum disulfide (MoS2) anti-galling coatings are applied to prevent cold welding.
Strategic fastener deployment across Hungary's strategic economic corridors: from the Pannonian geothermal basin to automotive clusters and chemical processing networks.
Hungary sits upon Europe's most abundant thermal reserves (Szeged, Miskolc). Subsurface brine extraction facilities experience aggressive H2S corrosion and high-temperature mineral deposits, demanding ASTM A194 Gr 7M and ASTM A182 heavy nuts with strict NACE MR0175 sour-service compliance.
Gigafactories and OEM automotive corridors in Debrecen, Győr, and Kecskemét mandate millions of certified Grade 8.8 and 10.9 high-clamp fasteners. Our automated optical-sorted nuts ensure zero defects on high-speed structural battery enclosure automated lines.
Refining complexes in Százhalombatta and Tiszaújváros require Class 300 to Class 2500 piping assemblies. Fasteners must maintain tight seals during cyclic thermal expansions, resisting volatile organic compounds, sulfur derivatives, and heavy hydrocarbon compounds.
Civil bridges, port cranes, and rail infrastructures along the Danube transport network experience high environmental moisture and winter de-icing salts. We supply hot-dip galvanized (HDG ISO 10684) and zinc-flake coated heavy hex nuts resistant to 1,500+ hours of neutral salt spray.
Comprehensive standard cross-reference chart to streamline technical requisitions for Hungarian procurement engineers and QA specialists.
| Material Grade | Governing Standard | Nominal Size Range | Proof Load Stress | Hardness Range | Primary Industrial Application |
|---|---|---|---|---|---|
| ASTM A194 Gr. 2H | ASME B18.2.2 / ASTM A194 | 1/2″ to 4″ (M12 – M100) | 175,000 psi (1,205 MPa) | 24 to 35 HRC | High-pressure steam, refinery flanges, pressure vessels |
| ASTM A194 Gr. 7 / 7M | ASME B18.2.2 / NACE MR0175 | 1/2″ to 3-1/2″ (M12 – M90) | 175,000 psi / 150,000 psi | 24-35 HRC / Max 22 HRC | H2S sour gas extraction, geothermal wells, subsea headers |
| ASTM A194 Gr. 8 / 8M | AISI 304 / 316 Austenitic | 1/4″ to 2-1/2″ (M6 – M64) | 80,000 psi (550 MPa) | 60 to 90 HRB | Chemical pipeline bypasses, food sanitization lines, cryogenic |
| EN 14399-4 (System HV) | European Standard (CE Marked) | M12 to M36 | 1,000 – 1,200 MPa | Class 10 (HRC 27 – 34) | Preloaded structural civil steelwork, gantry cranes, rail bridges |
| ISO 4033 / Class 10 | ISO Metric High Strength | M10 to M64 | 1,040 – 1,160 MPa | Class 10 / 12 | Automotive chassis fixtures, heavy hydraulic machinery, mining |
Combining three decades of precision forge manufacturing, rigorous European compliance credentials, and multi-modal container logistics into Central Europe.
Recognized as an Indian Boiler Regulations (IBR) and Engineers India Limited (EIL) approved manufacturer. Our quality systems adhere strictly to ISO 9001:2015, ensuring consistent metallurgical purity, certified grain structures, and zero non-destructive testing (NDT) rejection rates.
Every forging heat batch is analyzed with optical emission spectrometers, ultrasonic flaws detectors, Charpy V-notch impact rigs (tested down to -196°C for cryogenic services), and computerized tensile/proof-load testers before packing into seaworthy euro-pallets.
Regular containerized consolidated shipping routes through Port of Koper (Slovenia) and Rijeka (Croatia) ensure rapid rail-bonded customs delivery straight into Budapest, Debrecen, and Győr industrial warehousing, slashing delivery lead times.
Direct answers addressing technical standards, customs clearance, surface coatings, and mill certification queries.
Submit your line item bill of materials, engineering specs (ASME/EN/DIN), and required coating standards. Our technical sales desk will provide a full landed quotation within 12 hours.