
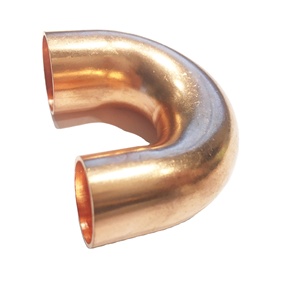
Girgaon, Mumbai, Maharashtra 400004, India [email protected] +91 9869506920

Buttweld Elbow Factories & Exporters for Melbourne

Technical Whitepaper & Procurement Compendium: High-Integrity ASME B16.9 and AS 4041 Compliant Buttweld Piping Solutions for Victorian Infrastructure, Refineries, and Hydrogen Corridors

Stock Portfolio

Engineered Pipeline Components & Buttweld Fittings

Precision-manufactured piping solutions certified to ASME, ASTM, and Australian standards. Fully traceable with EN 10204 3.1 certification for critical applications across Victoria.

1991 Manufacturing Excellence Since
11+ In-House NDT & Testing Units
100% Heat Traceable to EN 10204 3.1
98% Direct Melbourne On-Time In-Dock

1. Architectural Dynamics of Buttweld Elbows in Victorian Piping Infrastructure

As Australia accelerates its industrial decarbonisation, modernises municipal water processing assets, and expands heavy infrastructure throughout Greater Melbourne and the broader state of Victoria, the demand for highly reliable, seamless, and welded pipe fittings has reached unprecedented heights. Within continuous fluid conveyance, piping networks are subject to severe hydrostatic loads, fluid momentum fluctuations, corrosive marine atmospheric deposits, and thermal cycling. Under these operating conditions, the buttweld elbow serves as a fundamental piping component, directing pipeline trajectory while mitigating frictional hydraulic loss, turbulence-induced wall thinning, and localized stress risers.

In high-pressure processing facilities, mechanical integrity relies on continuous joint fusion. Unlike flanged or threaded joints, a precision-bevelled buttweld elbow undergoes complete butt-fusion welding with matching pipe spools. This establishes structural continuity, equalizes hoop stress capacity across the weld neck, and prevents galvanic cell formation under insulation. Sourcing buttweld elbows from certified manufacturers who maintain comprehensive forging, forming, and calibration workflows is therefore vital for procurement managers, pipeline integrity engineers, and engineering contractors operating out of Melbourne.

Hydraulic Geometry & Flow Dynamics

Long Radius (LR with R=1.5D) elbows minimize dynamic pressure drops in slurries and processing lines, whereas Short Radius (SR with R=1.0D) elbows fit tightly congested skid installations around Altona and Dandenong South plant footprints.

Strict Standard Compliance

Fabrication aligns with ASME B16.9, ASME B16.28, MSS SP-43, and the rigorous pressure-piping criteria of Australian Standard AS 4041. Material chemistries consistently comply with ASTM A234, ASTM A403, and ASTM A860 specifications.

High Integrity Weld Ends

Automated root face and land beveling to ASME B16.25 (37.5° ± 2.5° bevel with 1.6mm root face) ensures reliable robotic or orbital GTAW and SMAW penetration on pipeline spools.

2. Localised Application Scenarios Across Victoria

Victoria's varied industrial zones demand diversified material grades and fitting schedules to handle aggressive service conditions. Melbourne sits at the hub of Australia's maritime freight network and acts as the technical engineering center for complex onshore and offshore asset operations:

The Port Phillip & Westernport Marine Corridors: Industrial facilities and marine terminals along Port Phillip Bay face continuous exposure to airborne chlorides and marine spray. Desalination infrastructure in Wonthaggi, marine bunkering at Port Melbourne, and coastal wastewater discharge plants require buttweld elbows with superior pitting and crevice corrosion resistance. We routinely supply ASTM A403 WP316L, 2205 Duplex (UNS S31803/S32205), and 2507 Super Duplex (UNS S32750) elbows with controlled ferrite counts (35–55%) and guaranteed PREn ≥ 42 to prevent localized failure.

Altona, Geelong & Hastings Petrochemical Refineries: Downstream petrochemical plants, hydrocarbon fractionation facilities, and bulk fuel storage terminals rely heavily on heavy-wall carbon steel elbows (ASTM A234 WPB, WPC) and low-temperature carbon steels (ASTM A420 WPL6). These components undergo mandatory Charpy V-notch impact testing at -46°C to prevent brittle fracture during low-temperature upset events.

Latrobe Valley Energy Transformation & Circular Economy: As historical brown-coal generation transitions toward biomass, gas-peaking facilities, and industrial carbon abatement, power piping demands chromium-molybdenum alloy elbows. Our ASTM A234 WP11, WP22, and WP91 fittings withstand creep and microstructural graphitization up to 600°C under high steam pressures.

Gippsland Basin & Offshore Bass Strait Production: Subsea gas collection systems and landfall processing trains at Longford demand heavy-schedule, high-yield elbows certified to ASTM A860 (WPHY 52, WPHY 60, WPHY 65). These are sour-gas compliant per NACE MR0175/ISO 15156, featuring strict controls on HIC (Hydrogen-Induced Cracking) and SSC (Sulfide Stress Cracking).

Product Family Governing Standard Dimensional & Schedule Scope Standard Material Grades Inspection Matrix
ASME B16.9 Buttweld Elbows (45°, 90°, 180°) ASME B16.9 / AS 4041 / MSS SP-43 1/2″ to 48″ (DN 15 – DN 1200)
SCH 10S to SCH XXS
ASTM A234 WPB, WPL6, WP11, WP22; A403 WP304L, WP316L; 2205 Duplex 100% Dimensional CMM, Hydrostatic, RT/UT of welded seams, EN 10204 3.1
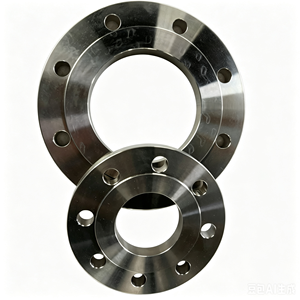
Forged High-Pressure Flanges ASME B16.5 / B16.47 / EN 1092-1 1/2″ to 60″ (Class 150 – 2500)
PN 6 to PN 400
ASTM A105N, A350 LF2, A182 F304L/F316L, F11, F51 Duplex MPI, Ultrasonic examination, Full PMI chemical validation
Small-Bore Forged Fittings ASME B16.11 / BS 3799 1/8″ to 4″ (Class 2000, 3000, 6000, 9000) ASTM A105, A182 F316L, A350 LF2, Nickel Alloys (Inconel 625, Monel 400) Hardness test (NACE MR0103/0175), Liquid Penetrant (DPI)
Engineered Heavy Fasteners ASTM A193 / A194 / AS 2528 M12 – M72 | 1/2″ – 3″ UNC Grades B7/2H, B8/8, B8M/8M, B16, L7/Gr. 7, Duplex 2205 Tensile elongation, Proof load verification, Salt spray corrosion metrics

3. Forward-Looking Infrastructure & Technical Trends Across Victoria

Melbourne's commercial, infrastructure, and heavy piping landscapes are undergoing generational transformation. Sourcing workflows for pipe fittings and buttweld elbows must adapt to shifting technological requirements:

Hydrogen Blending & H2-Ready Gas Infrastructure

Victoria's Renewable Gas Target and ongoing pilot projects across suburban Melbourne require low-permeability pipeline connections. Buttweld elbows intended for hydrogen-enriched natural gas (HENG) up to 20% H2 blend must feature ultra-low inclusion chemistries, minimal residual carbon equivalents (CE ≤ 0.38), and mirror-smooth internal surfaces to eliminate hydrogen embrittlement micro-voids.

Prefabricated Modular Process Skids

With high on-site unionized mechanical labor costs in Victoria, EPCs increasingly build modular skid assemblies in industrial workshop hubs like Campbellfield and Clayton. This elevates the demand for tight-tolerance, 100% calibrated buttweld elbows with laser-verified squareness and minimal ovality (≤ 1%) to speed automatic robotic orbital welding passes.

Stringent ESG & Low-Carbon Supply Chains

Tier-1 contractors across Melbourne's water utilities and transport infrastructure frameworks require audited Environmental Product Declarations (EPDs). Sourcing from facilities powered by energy-efficient induction heating with documented scrap-reclaim ratios helps meet corporate Scope 3 decarbonization mandates.

4. Manufacturer Integrity & Export Supply Advantages

Operating as a long-established Indian Government Recognized Export House since 1991, Rajtilak Metal serves as a reliable manufacturing bridge between premier forging yards and Melbourne's industrial engineering sectors. Our multi-decade track record ensures that Australian buyers avoid the compromises commonly associated with generic, untraced trading networks.

Our Mumbai manufacturing footprint features heavy hydraulic cold-forming mandrels, closed and open die drop hammers, modern heat-treatment furnaces, and multi-axis CNC machines. We produce seamless and welded buttweld elbows up to 48 inches alongside complementary ASME B16.5 flanges, forged socket-weld fittings, and high-tensile fastener packages.

EIL & IBR Institutional Approvals

Endorsed by leading international inspection agencies, including Engineers India Limited (EIL) and Indian Boiler Regulations (IBR). Our components regularly serve sour gas and high-pressure steam utility services across the Middle East, North America, and Australasia.

Unbroken Heat Traceability

Every buttweld elbow undergoes individual dot-peen or die-stamping detailing raw heat number, schedule wall thickness, material grade, and production lot. Full EN 10204 3.1 Mill Test Certificates guarantee direct traceability back to the original steel melt.

Specialized Melbourne Logistics

Sea-freight routes from Nhava Sheva (JNPT) directly to the Port of Melbourne offer consistent transit profiles (typically 18–22 days). All items are packed in heavy-duty, fumigated ISPM-15 export timber crates protected with inner waterproof liners and rust-inhibiting coatings.

Procurement Clarity

Frequently Asked Questions by Melbourne Sourcing Teams

Essential guidance addressing technical specifications, logistics, regulatory compliance, and testing for Australian engineering assets.

How do ASME B16.9 buttweld elbows align with the Australian Pressure Piping Code AS 4041?
AS 4041 explicitly accepts fittings manufactured to ASME B16.9, provided the design pressure/temperature ratings and material group design stresses correspond with recognized ASTM specifications (e.g., ASTM A234 for carbon/alloy steels, ASTM A403 for stainless). Wall thicknesses must match the calculated pipe schedule under AS 4041 design equations, accounting for the appropriate quality factor (E) and corrosion allowance.
Can mill test reports be validated by independent third-party inspectors before dispatch to Australia?
Yes. We routinely host third-party inspection agencies (TPIA) nominated by Australian clients—such as Bureau Veritas, DNV, SGS, Lloyd's Register, and TÜV. Inspections can cover dimensional verification, visual checks, liquid penetrant testing, radiography of welded seams, production mechanical tests, and Positive Material Identification (PMI) using handheld XRF analyzers.
What heat treatment is applied to stainless steel (e.g., WP316L) buttweld elbows after hot induction or cold forming?
All austenitic stainless steel elbows undergo full solution annealing post-forming, heating to 1040°C–1120°C followed by rapid water quenching. This dissolves chromium carbides back into the austenitic matrix, eliminating intergranular corrosion susceptibility near the bend throat and fulfilling ASTM A403 / AS 4041 requirements.
What are the typical lead times and maritime transit times to the Port of Melbourne?
Standard stocked carbon and stainless steel elbows can be packed and dispatched from Mumbai within 7 to 10 days of order confirmation. Bespoke heavy-wall schedules, custom radii, or exotic alloys (such as Alloy C276 or Inconel 625) typically require 3 to 5 weeks for manufacturing. Containerized maritime shipping from Nhava Sheva (JNPT) to Port Melbourne generally takes 18 to 24 days.
How are fittings protected against corrosion during maritime transit across equatorial zones?
Carbon steel and low-temperature fittings are thoroughly coated with heavy black bituminous varnish, clear anti-rust oil, or dry-film rust inhibitors based on client specifications. Stainless steel and duplex components are pickled, passivated, and wrapped in heavy-gauge polyethylene film. All orders are packed inside fumigated, ISPM-15 compliant timber cases containing active desiccants.

Collaborate with an Established Industrial Pipe Fitting Exporter

Whether you require standard ASME B16.9 elbows for immediate delivery in Melbourne, heavy-wall components for refinery upgrades in Altona, or specialized duplex alloys for marine projects around Westernport Bay, our engineering team delivers precision-manufactured, fully certified piping packages.

Send an Inquiry