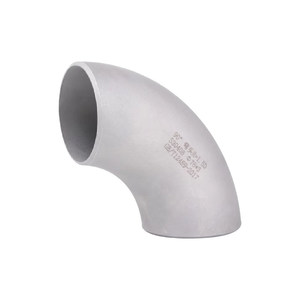
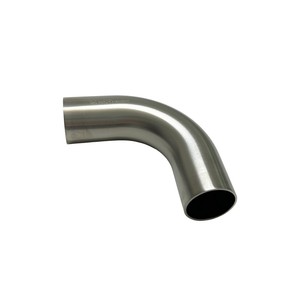
Precision-machined pipe fittings, forged high-pressure connectors, and industrial heavy-hex fastening elements manufactured for critical piping applications across Karachi, Lahore, Faisalabad, and Port Qasim.
The ASTM A403 specification governs wrought austenitic stainless steel piping fittings designed for pressure piping systems under ASME B31.1, B31.3, and B31.8 service conditions. Within this standard, Grade WP304L (UNS S30403) represents the low-carbon modification of standard 304, intentionally formulated with a maximum carbon threshold of 0.030%. This low carbon chemistry decisively inhibits chromium carbide precipitation along the austenite grain boundaries during welding and thermal cooling cycles. For plant engineers, maintenance directors, and EPC pipeline contractors operating in Pakistan, eliminating carbide precipitation ensures total immunity against intergranular corrosion (IGC) in the heat-affected zones (HAZ) of field-welded buttweld joints.
Our manufacturing and export operations strictly comply with both Class WP-S (seamless construction derived from prime seamless pipe or tube) and Class WP-W (welded construction manufactured from fully radiographed plate or welded pipe). To guarantee structural integrity, our cold-formed and hot-worked elbows, concentric reducers, eccentric reducers, equal tees, reducing tees, cross tees, and stub ends are subjected to full post-forming solution annealing at 1040°C to 1150°C, followed by rapid water quenching. This complete heat treatment dissolves any precipitate phases, restoring the austenitic microstructure to optimal corrosion resistance and mechanical ductility conforming to ASME B16.9 and MSS SP-43 dimensional tolerances.
| Property Parameter | ASTM A403 WP304L (Low Carbon) | ASTM A403 WP304 (Standard) | Engineering Benefit in Field Service |
|---|---|---|---|
| Carbon Content (Max %) | 0.030% Max | 0.080% Max | Prevents sensitization; eliminates post-weld solution annealing in field. |
| Chromium / Nickel Balance | 18.00% – 20.00% Cr / 8.00% – 12.00% Ni | 18.00% – 20.00% Cr / 8.00% – 10.50% Ni | Superior passivity layer stability in aggressive halide/chemical exposures. |
| Yield Strength (0.2% Offset) | 170 MPa (25,000 psi) Min | 205 MPa (30,000 psi) Min | High plasticity index; resilient against cyclic pressure pulsation. |
| Tensile Strength (MPa) | 485 MPa (70,000 psi) Min | 515 MPa (75,000 psi) Min | Robust tensile safety factor for severe process lines and water hammer. |
| Weldability Rating | Exceptional (GTAW/TIG, GMAW/MIG, SMAW) | Standard (Requires post-weld cooling control) | Drastically lowers welding turnaround time in Pakistani pipeline builds. |
As Pakistan accelerates modernization across heavy processing, petrochemical, and municipal infrastructure sectors, the requirement for reliably certified ASTM A403 WP304L butt-weld and forged fittings has grown exponentially. Engineers across local processing corridors specify WP304L to circumvent corrosion hazards arising from varied operational and climatic environments:
Urea, ammonia synthesis, and nitric acid manufacturing clusters around Multan, Sheikhupura, and Rahim Yar Khan require WP304L seamless buttweld 90° elbows, tees, and eccentric reducers. The low-carbon matrix provides absolute security against ammonium carbamate and nitric condensate corrosion.
Textile dyeing, wet bleaching, and chemical recovery plants encounter continuous contact with reactive dyestuffs, organic acids, and sodium silicate. ASTM A403 WP304L pipe fittings prevent localized pinhole leaks and pitting, sustaining continuous fabric production schedules without unscheduled line shutdowns.
Marine coastal environments along Karachi and Port Qasim demand external and internal corrosion protection. Hydrocarbon condensates, glycol dehydration spools, and cryogenic storage utility lines specify WP304L fittings to counter both coastal airborne chloride mist and product line corrosion.
Originally founded in 1991, Rajtilak Metal has grown into a premier Government of India recognized export house, manufacturing high-integrity piping components, forged flanges, and high-tensile fasteners under rigid global quality certifications.
Holding prestigious ISO 9001 quality management credentials, Engineers India Limited (EIL) approvals, and Indian Boiler Regulations (IBR) certifications, every single component exported to Pakistani clients is tagged with a distinct heat number stamped alongside physical MTC EN 10204 Type 3.1 verification sheets.

Over the past decade, piping procurement strategies in Pakistan have undergone a structural paradigm shift. Historically, local maintenance networks frequently relied on uncertified commercial grade "market 304" fittings sourced from unverified scrap rerolling channels. However, catastrophic pipe failures resulting from weld decay, wall-thickness thinning at outer elbow radiuses, and unpredictable pipe burst pressures have caused plant engineers to formally mandate strict compliance with ASME B16.9 and ASTM A403 specifications.
Key emerging drivers shaping the Pakistani piping ecosystem include:
Essential technical, regulatory, and commercial insights to simplify your import and project staging process.
WP304L keeps carbon below 0.030%, eliminating chromium carbide crystallization at weld boundaries. When welded in high-humidity or aggressive plant settings in Pakistan, the material retains full passivity without requiring post-weld solution heat treatment, thereby completely preventing weld line corrosion.
Every shipment is accompanied by a genuine EN 10204 3.1 Mill Test Certificate detailing 100% heat-specific spectral chemical analysis, tensile testing, yield points, elongation metrics, and Brinell/Rockwell hardness ratings. We also furnish hydrostatic or pneumatic test sheets and 100% X-ray / Radiographic Examination (RT) logs for welded lines upon request.
Yes. Our CNC machining lines produce ASME B16.9 buttweld and ASME B16.11 forged fittings across all standard schedules from SCH 5S, 10S, 40S, 80S, up to SCH 160 and XXS. We also produce custom-bore transitions designed to customer line drawings for smooth laminar flow without turbulent erosion.
Consignments are packed in heavy-duty, fumigated, ISPM-15 compliant sea-worthy wooden crates with moisture-barrier wrapping and durable end-caps to safeguard machined bevels against denting. Transit via major maritime sea freight directly to Karachi Port or Port Muhammad Bin Qasim offers optimized lead times.
Operating as an end-to-end forging and fabrication facility since 1991, our technical advantage is founded on comprehensive quality assurance, rigorous raw material selection, and extensive metallurgical expertise:
We forge exclusively from certified raw billets and seamless parent pipes sourced from tier-one stainless steel mills in India, South Korea, and Japan, guaranteeing clean melt structures devoid of internal inclusions.
Our facility houses 11 dedicated testing instruments including Oxford PMI analyzers, universal tensile machines, impact testing setups, and digital surface profile meters to audit roundness, ovality, and wall uniformity.
We streamline procurement by bundling ASTM A403 WP304L fittings with matching ASME B16.5 flanges, ASTM A193 B8/B8M stud bolts, and A194 Grade 8 hex nuts into consolidated, export-ready shipments.