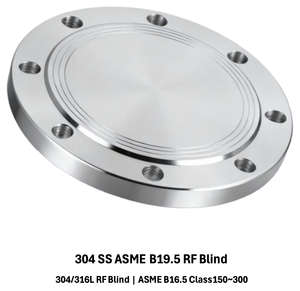

Engineered for extreme operating environments, severe shear fatigue, and thermal cycling across global upstream, refining, and chemical processing networks.
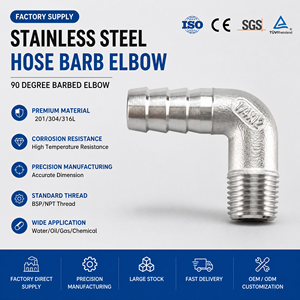
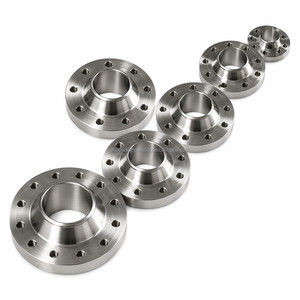
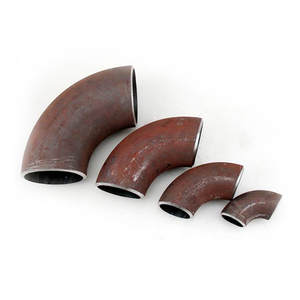
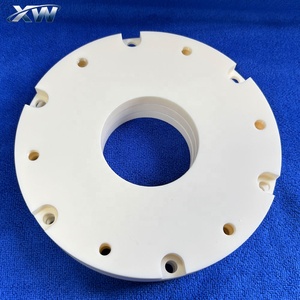
A 90-degree elbow is the most hydrodynamically critical structural fitting in any pressurized fluid pipeline, dictating directional momentum shifts, pressure drop gradients, and localized erosion profiles.
In standard ASME B16.9 and B16.11 specifications, Long Radius (LR) 90-degree elbows possess a centerline-to-face distance of 1.5 times the nominal pipe diameter. This gradual curvature suppresses cavitation zones and limits turbulent frictional loss across high-velocity multi-phase streams. Conversely, Short Radius (SR) elbows (1.0D) are engineered for critical spatial constraints, marine manifolds, and compact offshore skids where structural compactness outweighs fluidic resistance penalty.
Formed via hot-mandrel extrusion (Hamburg process) or cold-forming calibrated dies to ASTM A234 WPB or ASTM A403 WP316L, ensuring complete wall thickness uniformity without weld seams across high pressure pipelines.
Conforming to ASME B16.11 ratings in Class 3000, 6000, and 9000. Forged from solid billets (ASTM A105 / A182) for high-integrity small-bore lines, instrument takeoffs, and cyclic hydraulic circuitry.
Extending beyond austenitic stainless to Duplex 2205, Hastelloy C276, Inconel 625, and abrasion-resistant perforated alumina ceramic liners designed to withstand intense slurry erosion and aggressive chloride attack.
A reference architecture for EPC engineers and procurement teams to cross-reference nominal dimensions, metallurgy standards, and destructive test protocols.
| Component Category | Applicable Codes | Material Classifications | Nominal Size & Schedule | Mandatory QA/QC Verification |
|---|---|---|---|---|
| ASME B16.9 Butt Weld Elbow (90°/45°) | ASME B16.9, MSS SP-75, DIN 2605 | ASTM A234 WPB, WPC, A403 WP304L/316L, A860 WPHY 52/60/70 | 1/2″ NB to 48″ NB (SCH 10 to SCH XXS) | Bevel angle verification, ultrasonic wall thickness, radiography (RT), heat batch test |
| ASME B16.11 Forged Elbows (SW / NPT) | ASME B16.11, BS 3799, MSS SP-83 | ASTM A105, A350 LF2, ASTM A182 F316L, F11, F22 | 1/8″ NB to 4″ NB (Class 3000, 6000, 9000) | Liquid penetrant testing (PT), magnetic particle (MT), thread gauge verification |
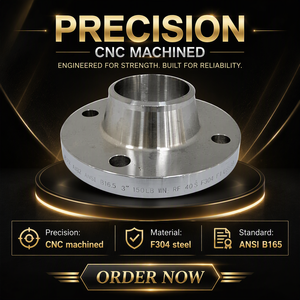
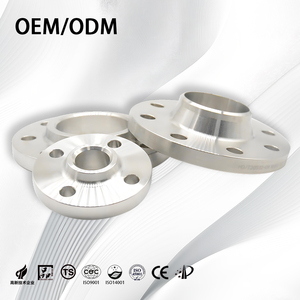
| ASME B16.5 / B16.47 Forged Flanges | ASME B16.5, EN 1092-1, BS 10 | ASTM A105, A182 F304/F316L, P235GH, 1.4404 | 1/2″ to 24″ (Class 150 - 2500), 26″ to 60″ (B16.47) | Serrated face micro-inch Ra profiling, PMI spectroscopy, tensile & Charpy V-notch |
| Engineered Ceramic & Special Hybrids | ISO 9001 Custom Specification | Alumina Ceramic 95%/99%, Silicon Carbide, Monel | Custom bore sizes, modular pipe liners | Vickers hardness, micro-porosity inspection, thermal shock resistance test |
The industrial pipe and fitting ecosystem is undergoing generational shifts driven by decarbonization, hydrogen transport, and automated supply chains.
Pipelines carrying high-pressure gaseous hydrogen demand sub-surface grain refinement and ultra-low sulfur metallurgy to resist hydrogen embrittlement (HE) and severe sulfide stress cracking under NACE MR0175/ISO 15156 standards.
With Europe’s Carbon Border Adjustment Mechanism (CBAM) enforcement, premier exporters now log the embodied scope-1 and scope-2 carbon footprint from the primary melt shop directly into digital mill certificates.
Hydraulic hot-extrusion now integrates closed-loop thermal sensors and automated tool wear monitoring, reducing wall thinning at the extrados of 90-degree elbows to under 3% compared to classical industry allowances.
Global supply disruptions have spurred EPC giants in the GCC and North America to shift from pure Just-In-Time procurement to regional strategic master distribution hubs for long-lead chrome-moly and nickel alloy fittings.
Operating as a Government of India Recognised Export House since 1991, our facilities merge metallurgical mastery with audit-ready documentation.
Our forged flanges, seamless buttweld 90° elbows, and high-tensile bolting lines hold accredited approvals across EIL (Engineers India Limited), IBR (Indian Boiler Regulations), and major international operators including ADNOC-tier requirements.
Each component undergoes laser-hard or deep-stamped marking detailing the primary melt heat number, pressure rating, material schedule, and manufacturer stamp, fully matched with an authentic EN 10204 3.1 inspection certificate.
Headquartered in Mumbai with direct access to JNPT port hubs, all export items are crated in bespoke, treated ISPM-15 compliant sea-worthy wooden cases, complete with end-protectors, desiccants, and anti-corrosion barrier coatings.
Addressing the core technical, compliance, and logistical inquiries faced by project managers and commercial procurement executives.
Contact our technical sales team for comprehensive bill-of-materials verification, project datasheets, MTC validation, and competitive global export pricing.
Send an Inquiry