
Manufactured to stringent ASME, ASTM, DIN, and API standards with complete heat-number batch traceability and third-party inspection compliance.
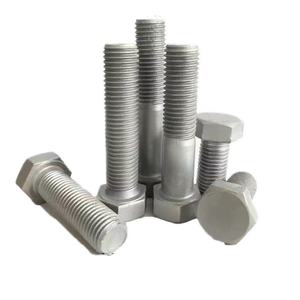
Engineered for extreme structural framing and high-pressure flange assemblies requiring superior shear resistance and anti-corrosion barrier protection.
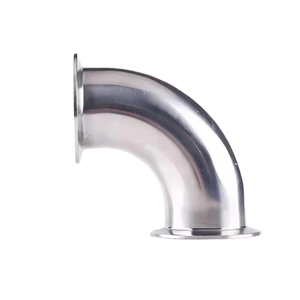
Ultra-clean surface finish Ra < 0.4µm for pharmaceutical and hygienic dairy applications with leak-free CIP/SIP sterilization capability.
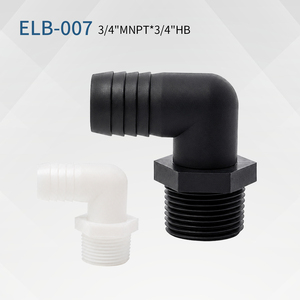
Precision-injection molded industrial nylon connectors featuring robust chemical resistance against mild acids, water cooling loops, and pneumatic systems.
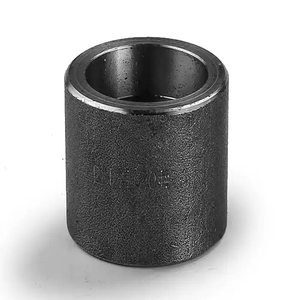
Certified ASTM A105 forged steel coupling for high-vibration oil, refinery gas, and high-pressure steam distribution headers.
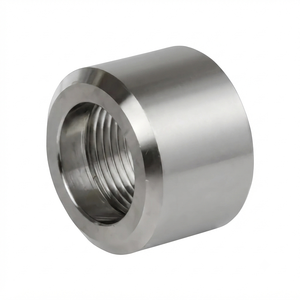
CNC machined NPT/BSPT threaded ports engineered for precise instrumentation tapping, drain plugs, and thermowell installations.
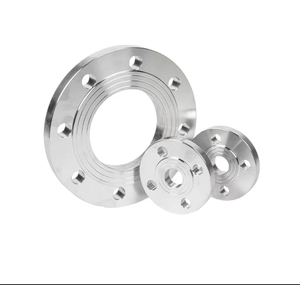
Closed-die forged weld neck, blind, and slip-on flanges with RTJ or RF serrated faces complying with API 6A and ASME B16.5.
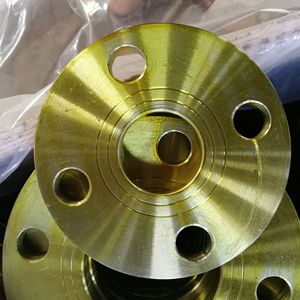
Designed for ballast systems, marine utilities, and municipal wastewater lines where cost efficiency meets strict JIS dimensional accuracy.
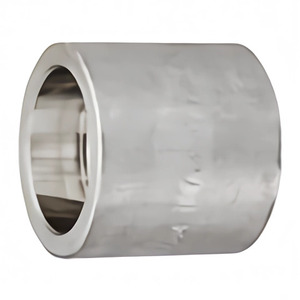
Heavy-wall Class 3000/6000 socket-weld fittings delivering maximum fatigue resistance against turbulent fluid dynamics and pressure hammers.
In high-pressure piping architectures, the pipe cap (or end closure) represents one of the most mechanically stressed pressure-boundary elements. Unlike steady inline conduit flows, blind terminations experience intense perpendicular hydraulic thrust, severe cyclic fluid hammer, and localized hoop stress concentrations. As an premier OEM/ODM pipe cap supplier and global exporter, Rajtilak Metal integrates deep metallurgical science with cold deep-drawing, hot spinning, and closed-die forging technologies to produce end caps that surpass the design limits of ASME B16.9 (factory-made buttweld fittings) and ASME B16.11 (forged socket weld and threaded connections).
The structural integrity of a pipe cap depends critically on its ellipsoidal aspect ratio and knuckle radius transition. Under internal fluid loading, abrupt cross-sectional shifts invite catastrophic stress concentration. Our engineering matrix utilizes advanced Finite Element Analysis (FEA) to verify that wall thinning at the apex (crown) remains well above design code allowances (such as ASME Boiler and Pressure Vessel Code Section VIII Division 1). Whether manufacturing hemispherical heads for ultra-high-pressure subsea manifolds, 2:1 semi-ellipsoidal caps for petrochemical transmission, or torispherical closures for moderate industrial storage, our closed-loop thermal treatment ensures uniform grain structure, completely relieving residual forming stresses.
| Standard / Category | Available Size Matrix | Pressure Class / Wall Schedule | Metallurgical Grades & Standards | Quality Verification & Testing |
|---|---|---|---|---|
| ASME B16.9 Buttweld Caps | 1/2" to 60" (DN15 – DN1500) | SCH 10S, 40S, 80S, XS, SCH 160, XXS | ASTM A234 WPB, WPC; ASTM A403 WP304/304L, WP316/316L, 904L; Duplex 2205; Super Duplex 2507 | 100% Radiographic Testing (RT) / UT, Hydrostatic Test, EN 10204 3.1 MTC |
| ASME B16.11 Forged Caps | 1/8" to 4" (DN6 – DN100) | Class 2000, 3000, 6000, 9000 (Threaded / SW) | ASTM A105, A350 LF2 Class 1/2; ASTM A182 F11, F22, F51, F53, F55; Inconel 625, Hastelloy C276 | PMI Spectrometry, Wet Magnetic Particle (MPI), Liquid Dye Penetrant (PT) |
| MSS SP-75 High-Yield Caps | 16" to 56" (DN400 – DN1400) | WPHY 42, WPHY 52, WPHY 60, WPHY 65, WPHY 70 | High-strength low-alloy micro-alloyed carbon steel for sour crude & natural gas cross-country pipelines | Charpy V-Notch Impact Test at -46°C, HIC & SSCC Resistance (NACE MR0175) |
| Sanitary & Tri-Clamp Caps | 1/2" to 12" | Low Pressure / Sanitary Vacuum | AISI 304, 316L Electro-Polished (EP) | Surface Roughness Ra < 0.38µm (15µin), Ferrite Scope Inspection, 3A & FDA Validated |
How international EPCs, supply chain directors, and chemical operators are restructuring vendor qualification and lifecycle costing.
Global procurement teams no longer accept single-compliance fittings. Future-proof piping systems mandate dual-certified grades (e.g., 304/304L or 316/316L with low-carbon corrosion immunity and high-yield mechanical values) and dual-standard approvals bridging ASME B16.9 with European EN 10253-2 and DIN specs to reduce international inventory overhead.
Physical mill paperwork is rapidly transitioning to cloud-linked QR-code laser matrix marking directly on the pipe cap rim. Procurement protocols for offshore ADNOC, Saudi Aramco, and European offshore wind networks now require immutable digital traceability directly connecting each heat number to original molten billet chemical spectrometry.
With the surge in Liquefied Natural Gas (LNG) liquefaction facilities and green hydrogen pilot infrastructure, procurement parameters are heavily weighted toward deep sub-zero impact toughness down to -196°C and strict austenitic grain size controls (ASTM 5 or finer) to eliminate micro-cracking and hydrogen embrittlement risks.
Transitioning from conventional hot stamping to smart hydraulic hydroforming and CNC compound weld prep automation.
Modern orbital automatic pipeline welding mandates extreme tolerances on the buttweld prep. Our advanced multi-axis CNC machines deliver J-bevels, V-bevels, and specialized compound bevel transitions with razor-thin root face variations within ±0.2mm, dramatically accelerating field-joint fit-up speed.
Traditional thermal pressing frequently causes unacceptable knuckle thinning. By adopting high-tonnage servo-hydraulic cold hydroforming with synchronized die counter-pressures, our plant achieves uniform nominal wall retention across the entire contour, reducing deadweight while enhancing pressure thresholds.
To eliminate surface scale and decarburization during post-forming heat treatments, automated continuous solution annealing furnaces with computerized nitrogen/argon protective atmospheres guarantee uniform hardness under 22 HRC in compliance with NACE MR0175 sour service mandates.
A Government of India Recognised Export House delivering engineered pipe components to global operators since 1991.
Officially vetted and approved by Engineers India Limited (EIL) and the Indian Boiler Regulations (IBR). Our production workflows strictly follow ISO 9001 quality systems with extensive supply credentials for ADNOC-compliant projects across the Middle East.
Equipped with 11 in-house testing units, including optical emission spectrometers for PMI, 1000kN universal tensile testers, Charpy impact pendulums (-196°C), intergranular corrosion test setups, and hydrostatic test bunkers reaching up to 15,000 PSI.
Substantial inventory holding in prime carbon steel (A234 WPB, A105, A350 LF2), stainless (304L, 316L, 904L), chrome-moly alloy steel (WP11, WP22), and high nickel superalloys (Inconel, Monel, Hastelloy) with swift port-dispatch to the Middle East, Southeast Asia, Europe, and the Americas.
Direct technical answers to questions routinely submitted by project engineers, QA/QC inspectors, and buying agents.