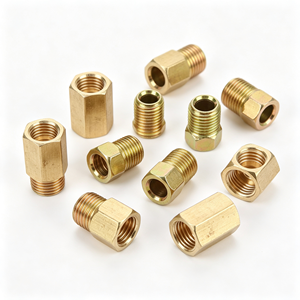
The integrity of modern oil, gas, chemical, petrochemical, and power generation networks hinges on precision-engineered buttweld fittings capable of withstanding extreme cyclic stress, cryogenic shocks, and aggressively corrosive chemical media. As a primary ASME B16.9 Fittings Factory and Global OEM/ODM Supplier, Rajtilak Metal integrates advanced metallurgical science, precision die forging, and automated CNC machining to deliver piping components that exceed regulatory and operational benchmarks. Operating since 1991 from our advanced manufacturing bases, we support EPC engineering contractors, worldwide stockists, and processing facilities with fully certified, heat-traceable ASME B16.9 fittings, ASME B16.5 flanges, forged high-pressure branch connections, and high-tensile bolting solutions.
Seamless and welded buttweld elbows, reducing tees, flanges, olets, and bolting configurations precision-machined to ASME, ASTM, and DIN standards.
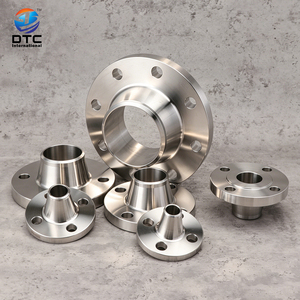
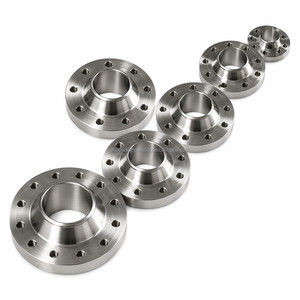
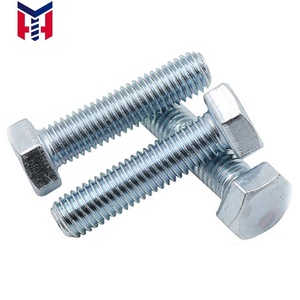
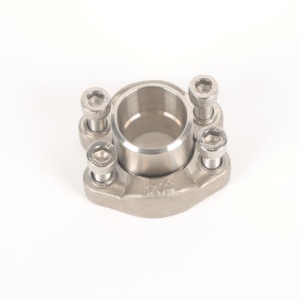
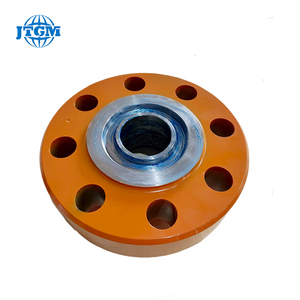
Decades of manufacturing discipline verified by international certifications, government recognitions, and strict metallurgical testing procedures.
Operating since 1991 as an officially recognized Indian Export House, Rajtilak Metal delivers comprehensive export crating, international logistics compliance, and direct vendor code approvals across major national oil companies including ADNOC-specified projects.
Our complete line of forged fittings, flanges, and piping bends complies with Engineers India Limited (EIL) and Indian Boiler Regulations (IBR) standards, validating mechanical resilience under high steam pressure and destructive thermal expansion cycles.
Every single buttweld fitting and forged component is electro-chemically or laser-marked with heat number, size, wall schedule, and material grade. Fully digitized Mill Test Certificates (MTCs) verify spectral chemistry, tensile yields, and Charpy V-notch impacts.
From custom branch fittings, high-yield heavy-wall elbows (ASTM A860 WPHY 60/65/70), to non-standard reducing crosses and split flanges, our multi-axis CNC lathe centers execute bespoke client blueprints within micro-millimeter dimensional tolerances.
We source prime billet ingots, forging round bars, and heavy-gauge mother pipes exclusively from vetted Tier-1 steel producers across India, South Korea, and Japan, avoiding low-cost unverified scrap melts and ensuring structural homogeneity.
In addition to standard ASTM A234 WPB and stainless 304L/316L, we engineer components in Duplex 2205, Super Duplex 2507, Inconel 625, Hastelloy C-276, Monel 400, and Grade 2 Titanium for cryogenic LNG, offshore seawater, and sour acid environments.
Standardized dimensional envelopes, pressure-temperature ratings, and applicable ASTM/ASME material specifications for industrial piping designers.
| Product Family | Governing Standard | Size Envelope | Wall Schedule / Class | Standard & Exotic Alloys |
|---|---|---|---|---|
| Buttweld Elbows (45°, 90°, 180°) | ASME B16.9 / MSS SP-75 | 1/2″ to 48″ (Seamless to 24″) | SCH 10S through SCH XXS | ASTM A234 WPB/WPC, WP11, WP22, A403 WP304L/316L, A860 WPHY 52/60/65/70 |
| Equal & Reducing Tees | ASME B16.9 / DIN 2615 | 1/2″ to 48″ | SCH 5S to SCH 160 / XXS | ASTM A420 WPL6 (Low-Temp), Duplex 2205 (S31803), Super Duplex 2507 (S32750) |
| Concentric & Eccentric Reducers | ASME B16.9 / MSS SP-43 | 1/2″ to 60″ | Standard / Extra Heavy | Nickel 200, Monel 400, Inconel 600/625, Incoloy 800/825, Hastelloy C276 |
| Branch Weldolet & Sockolets | ASME B16.11 / MSS SP-97 | 1/8″ to 24″ (Run Pipe) | Class 3000, 6000, 9000 | ASTM A105, A350 LF2, A182 F304L/F316L/F51/F53, AISI 4130 |
| Industrial Pipe Flanges | ASME B16.5 / B16.47 Ser. A/B | 1/2″ to 60″ | Class 150 to 2500 LBS | Forged Carbon Steel, Stainless Steel, P235GH, P250GH, 1.4404, Titanium Gr. 2 |
| High-Tensile Studs & Nuts | ASTM A193 / A194 / ISO 898 | M12 to M72 (1/2″ to 3″) | Grade 8.8, 10.9, 12.9 | A193 B7/B7M/B8/B8M, A194 Gr. 2H/7/8/8M, Duplex, Inconel Bolting |
How digital metallurgy, decarbonization protocols, and supply chain regionalization are transforming high-pressure piping specifications.
The global energy transition is mandating fittings engineered specifically to mitigate High-Temperature Hydrogen Attack (HTHA) and Hydrogen Embrittlement. Modern piping procurement requires ultra-low phosphorus and sulfur chemistry (P ≤ 0.010%, S ≤ 0.005%) along with NACE MR0175/ISO 15156 hardness verification below 22 HRC across weld heat-affected zones.
Procurement teams are shifting away from paper-based certs toward encrypted digital documentation. By binding QR codes and laser-etched heat identifiers directly to digital inspection records, contractors gain instantaneous field verification of Charpy impact results, hydro-testing pressure graphs, and positive material identification (PMI).
Traditional hot-slug pushing is increasingly augmented by automated cold-mandrel hydraulic extrusion for stainless and duplex buttweld elbows. This process guarantees micro-structural grain alignment, prevents surface decarbonization, and minimizes ovality deviations to well within one-third of the allowable ASME B16.9 threshold.
Direct technical answers addressing standards compliance, third-party inspection, wall schedule variations, and export packaging.