Seamless and welded concentric reducers, forged flanges, custom elbows, and heavy-duty industrial fasteners certified to international standards with complete heat-melt traceability.
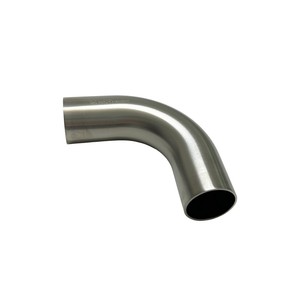
Analyzing critical wall thickness transitions, fluid turbulence reduction, and metallurgical stress tolerance in high-pressure petrochemical, LNG, and supercritical power systems.
In high-velocity process piping networks, concentric reducers are vital transition fittings manufactured with symmetric, cone-shaped geometry where both pipe centerlines share an identical axis. Unlike eccentric reducers that prevent gas pockets in horizontal pump suctions, concentric reducers are engineered specifically for vertical flow orientations and pressurized headers where balanced velocity distribution and uniform fluid dynamics are non-negotiable. As global energy, subsea, and refining projects operate under increasingly severe mechanical stresses, procurement engineers require custom OEM concentric reducers designed to mitigate cavitation, minimize pressure drop gradients, and eliminate hoop stress concentrations across non-standard wall schedules.
Standard catalogue fittings manufactured via conventional stamping often suffer from localized wall thinning along the transitional knuckle radius. At Rajtilak Metal, our custom OEM concentric reducer manufacturing employs multi-axis CNC hydroforming, hot induction swaging, and calibrated cold squeezing techniques. By modeling wall-thinning coefficients using Finite Element Analysis (FEA), we ensure that post-forming wall thicknesses meet or exceed ASME B16.9 minimum allowable limits across both large end (nominal diameter D1) and small end (nominal diameter D2).
Whether handling volatile natural gas at Class 2500 ratings or aggressive chemical acids, each component undergoes precision machining of weld bevel ends to ASME B16.25 standards, enabling automated orbital welding and superior radiographical weld pass integrity.

Comprehensive standard coverage engineered for extreme thermal gradients, cryogenic ductility, and sour service corrosion prevention.
| Material Family | Applicable ASTM / ASME Grades | Size Range (NPS) & Schedules | Primary Service Application | Yield Strength & Hardness Limit |
|---|---|---|---|---|
| Austenitic Stainless Steel | ASTM A403 WP304/304L, WP316/316L, WP321, 904L | 1/2″ to 48″ (SCH 10S to SCH XXS) | Cryogenics, LNG Processing, Chemical Acids, Food & Pharma | Yield ≥ 205 MPa | Max Hardness ≤ 217 HBW |
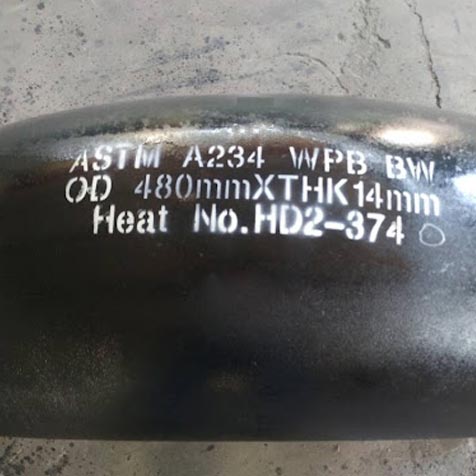
| High-Yield Carbon Steel | ASTM A234 WPB, WPC; ASTM A860 WPHY 52 / 60 / 65 / 70 | 1/2″ to 60″ (SCH 40 to SCH 160) | High-Pressure Hydrocarbon Transmission, Sour Service (NACE MR0175) | Yield 360 to 485 MPa | Hardness ≤ 22 HRC |
| Duplex & Super Duplex | ASTM A815 UNS S31803, S32205, S32750 (2507) | 1/2″ to 36″ (SCH 10S to SCH 80S) | Offshore Platforms, Seawater Desalination, High Chloride Media | PREN ≥ 42 | Yield ≥ 550 MPa | Charpy V-Notch Tested |
| Low-Temperature Steel | ASTM A420 WPL6 / WPL3 | 1/2″ to 36″ (SCH STD to SCH 160) | Refrigeration, Sub-Zero Cryogenic Gas Plants (-46°C to -101°C) | Impact Energy ≥ 27 J at -46°C |
| Chrome-Moly Alloy Steel | ASTM A234 WP11, WP22, WP91, WP92 | 1/2″ to 32″ (SCH 40 to SCH XXS) | Supercritical Steam Headers, Refinery Reforming Units | Creep-Resistant up to 600°C | 100% UT Inspected |
| Nickel Alloys & Titanium | Inconel 625, Hastelloy C-276, Monel 400, Titanium Gr. 2/5 | 1/2″ to 24″ (Custom Heavy Wall) | Severe Flue Gas Desulfurization, Chlorine Processing, Marine Subsea | Extreme Pitting/Crevice Resistance | Heat Treated |
How digital supply networks, carbon neutrality mandates, and modular construction paradigms are transforming global MRO and EPC purchasing decisions.
Global EPC contractors now reject non-verifiable test certificates. Future tenders prioritize manufacturers utilizing direct QR-coded laser-etched heat identifiers linked directly to cloud-based EN 10204 3.1 & 3.2 inspection dossiers, ensuring instantaneous validation of melt origin, Charpy impact toughness, and PMI spectral readings.
Procurement teams across the European Union, the Middle East, and North America are actively tracking Scope 3 embodied carbon. Sourcing strategies are pivoting toward manufacturers who source prime billets forged with Electric Arc Furnace (EAF) scrap-recycled routes and renewable-powered heat treatment furnaces.
To slash onsite installation hours and field welding costs, EPCs are shifting away from standalone loose fittings toward factory-prefabricated transition assemblies. Custom OEM concentric reducers integrated directly with forged weld neck flanges or calibrated branch connections reduce field NDT failure rates by over 40%.
From hydroforming automation to corrosion-resistant internal overlay cladding, engineering methods are evolving to meet extreme hydrogen and deepwater environments.
Advanced cold drawing with continuous hydraulic feedback eliminates wall wrinkling, providing an exceptionally uniform wall profile without grain shear.
Automated hot wire TIG cladding lines allow cost-effective carbon steel reducers to be lined with 3mm Inconel 625 for extreme sour gas (H2S) service.
Automated multi-probe ultrasonic immersion scanning maps 100% of the transitional surface to verify compliance with strict pipeline tolerance bands.
Controlled solution annealing and nitrogen quenching optimize microstructural austenite-ferrite phases, resisting HIC and SSC under 100 bar pure H2.
Decades of proven export performance backed by rigorous quality accreditations and premier EPC engineering approvals.
Established in 1991 in Mumbai, Rajtilak Metal has grown into a Government of India Recognised Export House delivering engineered buttweld fittings, forged flanges, and high-tensile fasteners to world-scale offshore, chemical, refining, and desalination projects across 30+ countries.
Operating with Indian Boiler Regulations (IBR) approval and Engineers India Limited (EIL) certification, our supply history encompasses prestigious international ventures including ADNOC-approved oil & gas projects throughout the Middle East, EPC contracts in Southeast Asia, and major infrastructure installations in Europe and North America.
Official status providing priority international customs clearance, rapid multimodal sea/air logistics, and seaworthy fumigated wooden crate packaging.
Unrestricted access for client-appointed inspectors including Lloyd's Register, DNV-GL, TÜV Rheinland, Bureau Veritas, and SGS prior to dispatch.
Readily available inventories in 304L, 316L, Duplex 2205, A105, A234 WPB, and high-tensile alloy stud bolts allowing 48-hour turnarounds on urgent MRO shutdowns.
Addressing critical technical considerations, wall thickness calculations, hydrotesting standards, and international order fulfillment protocols.
Consult with our engineering metallurgists, request immediate line-item tender quotations, or submit custom component drawings for certified OEM production.
Inquire Now