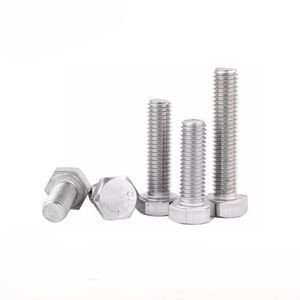
Explore our core export-grade industrial inventory, manufactured in strict compliance with ASME, ASTM, DIN, and EN industrial specifications.
A comprehensive technical analysis of bolted joint design, alloy selection, and mechanical behavior under extreme thermomechanical loads.
In high-pressure piping assemblies and pressurized flange joints (ASME B16.5 / B16.47), continuous all-thread stud bolts (often designated as Stud Bolts for Pressure-Temperature Piping) are preferred over standard hex head bolts. Continuous threading ensures uniform cross-sectional stress distribution along the entire grip length, eliminating the localized notch concentration common at the shank-to-head transition under thermal cyclic expansion.
Engineered for high-pressure boilers, refineries, and pressure vessel service where operational temperatures exceed 400°C (752°F).
Specifically formulated for low-temperature containment, LNG liquefaction terminals, and sub-zero Arctic infrastructure.
For aggressive offshore topsides, chloride-rich splash zones, subsea manifolds, and chemical leaching autoclaves.
| ASTM Grade | Base Metallurgy | Heat Treatment Protocol | Tensile Strength (Min) | Yield Strength (Min) | Recommended Nut Pairing |
|---|---|---|---|---|---|
| ASTM A193 B7 | AISI 4140/4142 Cr-Mo Steel | Quenched & Tempered (≥ 593°C) | 125 ksi (860 MPa) | 105 ksi (720 MPa) | ASTM A194 Grade 2H |
| ASTM A193 B7M | AISI 4140/4142 Cr-Mo Steel | Q&T with Controlled Tempering | 100 ksi (690 MPa) | 80 ksi (550 MPa) | ASTM A194 Grade 2HM |
| ASTM A320 L7 | AISI 4140 Cr-Mo Alloy | Liquid Quenched & Tempered | 125 ksi (860 MPa) | 105 ksi (720 MPa) | ASTM A194 Grade 7 / 7L |
| ASTM A193 B8 Cl.2 | AISI 304 Austenitic Stainless | Solution Annealed & Strain Hardened | 125 ksi (860 MPa) [up to 3/4"] | 100 ksi (690 MPa) | ASTM A194 Grade 8 |
| ASTM A193 B8M Cl.2 | AISI 316 Austenitic Stainless (Mo) | Solution Annealed & Strain Hardened | 110 ksi (760 MPa) [up to 3/4"] | 95 ksi (655 MPa) | ASTM A194 Grade 8M |
| UNS S32750 | 25Cr-7Ni-4Mo-0.28N Super Duplex | Solution Annealed & Rapid Quench | 116 ksi (800 MPa) | 80 ksi (550 MPa) | UNS S32750 Heavy Hex Nut |
Combining three decades of precision forging, state-of-the-art cold and hot roll threading, and uncompromising European-standard testing regimes.
Every single metric ton of round bar feedstock is exclusively procured from top-tier, certified steel mills in India, South Korea, and Japan. We maintain 100% lot traceability:
We do not rely on third-party approximations. Our laboratory infrastructure guarantees zero non-conformance prior to container loading:
Corrosive subsea, chemical vapor, and marine splash-zone environments demand high-performance barrier layers:
How global EPCs, supply chain directors, and asset operators are navigating the next decade of decarbonization, digital trace, and total joint validation.
Procuring flanges, buttweld fittings, gaskets, and stud bolts from disjointed suppliers creates systemic joint liability. The market is shifting to bundled packages:
With the European Union Carbon Border Adjustment Mechanism (CBAM) fully taking shape, global importers face carbon emissions reporting obligations:
Manual PDF-based Mill Test Certificates are becoming obsolete. Project procurement requires verifiable digitized authentication:
From work-hardening thread profiles to next-generation dry-film galling prevention, manufacturing is evolving to eliminate field failure.
Cutting threads with a cutting tool cuts across the natural grain structure of the steel bar, creating microscopic fissures and stress-concentration root notches. In contrast, hydraulic cold thread rolling plastically displaces metal along burnishing dies. This preserves uninterrupted grain flow lines parallel to the thread profile, creates smooth root radii, and induces beneficial compressive residual stresses that increase bolt fatigue life by more than 300% under cyclical vibratory conditions.
Austenitic stainless steels (ASTM A193 B8, B8M) have a high tendency for galling (friction cold-welding) during pneumatic torqueing. New production lines incorporate molybdenum disulfide (MoS2) and specialized nano-ceramic base coats that eliminate galling without requiring messy grease compounds on-site.
Uniformity in hardness and grain size is paramount for ASTM A193 Grade B7 and ASTM A320 Grade L7 fasteners. Our continuous mesh-belt furnace lines utilize automated nitrogen-methanol endothermic atmospheres to prevent surface decarburization, ensuring consistent 100% core-to-surface metallurgical hardness.
To eliminate dimensional thread pitch error, out-of-roundness, and burrs, high-speed 360-degree multi-camera optical sorters inspect 100% of finished studs prior to packing. Pitch diameter, major diameter, and chamfer angles are validated against ASME B1.1 Class 2A tolerances automatically.
Straightforward technical answers to the most common engineering, metallurgical, and shipping inquiries.
Direct export pricing, complete EN 10204 3.1 material test certificates, third-party inspection coordination (SGS, TÜV, BV, DNV), and prompt global ocean/air freight handling.
Send an Inquiry